English

When evaluating indoor full color led display manufacturers, the practical decision always comes down to locking the physical bill of materials (BOM) before wiring a production deposit rather than negotiating purely on price per square meter. If you need a direct engineering recommendation upfront: for corporate boardrooms, broadcast studios, church sanctuaries, retail flagships, and auditoriums, your safest baseline is a 320mm × 160mm or 250mm × 250mm module utilizing Nationstar or Kinglight copper- or gold-wire LEDs (SMD2121, GOB, or Flip-Chip COB depending on pitch), driven by dedicated pulse-width modulation (PWM) constant-current driver silicon (such as the Macroblock MBI5153 or Chipone ICN2153) operating at 1/16 or 1/32 scan, assembled on a 1.6mm 4-layer FR-4 TG170 printed circuit board with at least 1.5oz copper weight, and magnetically mounted onto CNC-machined die-cast aluminum frames. Bypassing generic export trading companies in favor of audited OEM/ODM factories in Shenzhen's Bao'an or Guangming districts that provide contractual single-bin diode lot matching and documented 72-hour continuous thermal burn-in is the only reliable way to prevent patchy color stepping, catastrophic driver chip burnouts, and costly service callouts.
Below is an exhaustive, real-world engineering teardown, factory audit framework, and procurement guide to help AV integrators, display rental operators, and commercial contractors source indoor full color LED displays directly from overseas manufacturing lines with complete technical certainty.
Picture this situation: your integration firm lands a contract to install an 8×4 meter indoor video wall for a corporate auditorium or high-end hotel ballroom. You bypass domestic distributors who mark up hardware by 40%, head directly to overseas wholesale platforms, and locate a vendor in Bao'an offering P2.0 indoor panels for an unbelievable $18 per module.
The digital specification sheet looks pristine. The brochure boasts 3,840Hz refresh rate, 800 nits brightness, high contrast, and a three-year factory warranty. The single sample tile they courier to your office looks razor-sharp on your workbench. You wire the 30% production deposit, wait six weeks for ocean transit, build the ground-support frame, and commission the video wall.
For the first ninety days, everything runs fine. Then seasonal temperature shifts kick in.
Under sustained daily operation in an air-conditioned room where ambient temperatures fluctuate between events, you notice faint color blocks appearing across adjacent panels. When showing a clean corporate white or light grey presentation slide, the screen looks like a patchwork quilt: some panels tint slightly yellow-green, while others shift toward magenta. By month six, individual blue diodes begin to fail in random vertical streaks, and during live events, attendees recording the stage with smartphones see dark rolling scan lines across the image.
Suddenly, you are spending hundreds of dollars a visit on technician labor, pulling modules, replacing driver chips, and desperately trying to keep a client from withholding their final retention payment.
The modules did not fail by random bad luck. They failed because indoor full color LED manufacturing in China is deeply stratified. In industrial centers like Shiyan, Fuyong, and Guangming, two modules that look identical from five feet away can have a 200% variance in raw component costs. When you understand where factory assemblers strip out build costs, you stop shopping for cheap price tags and start shopping for engineering specifications.
To evaluate any quotation from an overseas manufacturer, you must strip the module down into its foundational mechanical and electronic subsystems. When we are using these panels on commercial job sites, this is the internal architecture that separates industrial workhorses from budget toys:
+-------------------------------------------------------------+
|               Indoor Full Color LED Subsystems              |
+-------------------------------------------------------------+
| [Face Mask]      Anti-Glare Polycarbonate with Shading Fins |
| [LED Emitters]   SMD / GOB / COB / MIP (Nationstar/Kinglight)|
| [PCB Substrate]  1.6mm 4-Layer FR-4 (TG170, ≥1.5oz Copper)  |
| [Driver Silicon] High-Refresh Constant Current PWM ICs      |
| [Housing Base]   Reinforced ABS/PC Structural Chassis       |
| [Power / Data]   Gold-Plated 16-Pin IDC + VH4 5V DC Post    |
+-------------------------------------------------------------+
The light-emitting diode is the single largest cost driver in the bill of materials, accounting for 40% to 60% of total module cost:
Surface-Mount Devices (SMD2121 / SMD1515 / SMD1010): The traditional industry standard. Individual lamp beads are reflow-soldered to copper pads. Gold wire (Au) bonding provides maximum ductile fatigue resistance during thermal expansion cycles (-20°C to +60°C). Copper wire (Cu) offers a solid commercial balance, provided the packaging house maintains strict inert nitrogen gas shielding during bonding. Alloy or silver wire is a high-risk budget shortcut that leads to sulfur-induced blackening and micro-cracking within two years.
Glue-on-Board (GOB): Standard SMD boards coated under vacuum with an optically clear, high-durability epoxy or polyurethane resin. This creates an impact-resistant, dust-proof, and moisture-sealed front surface (Shore D 60+ hardness). GOB is ideal for high-traffic retail spaces, school auditoriums, and rental screens where crew members frequently bump tile corners.
Chip-on-Board (COB) & Flip-Chip COB: Microscopic semiconductor dies are bonded directly to the PCB substrate without packaging lead frames, then cast under optical resin. Flip-Chip COB eliminates bond wires entirely, dropping pixel failure rates to below 5 PPM (parts per million). It provides extreme 10,000:1 contrast ratios and runs significantly cooler, making it the preferred standard for fine-pitch control rooms and corporate boardrooms under P1.5.
Micro-in-Package (MIP): An emerging architecture where micro-LED dies are packaged into individual microscopic surface-mount carriers before automated SMT placement. MIP allows manufacturers to test and bin micro-diodes before soldering, avoiding the expensive yield loss of full COB boards while delivering exceptional optical contrast.
The driver chip dictates refresh rates, grayscale depth, and low-brightness color fidelity:
Basic Latching Registers (generic 74HC595 derivatives or unbranded clones): Found in entry-level, rock-bottom displays. They lack dedicated pulse-width modulation (PWM) memory, top out at sub-960Hz refresh rates, show dark horizontal scan lines on phone cameras, and crush dark gray tones into blotchy black patches.
Dedicated PWM Constant Current Drivers (e.g., Macroblock MBI5153, MBI5252, or Chipone ICN2153, ICN2069): Essential for commercial signage, broadcast spaces, and corporate video walls. These ICs deliver true 3840Hz to 7680Hz refresh rates, smooth 14-bit to 16-bit grayscale depth, low knee-voltage operation (0.2V to 0.4V), and integrated hardware circuits that eliminate ghosting, open-circuit cross lines, and caterpillar artifacts caused by shorted LEDs.
An indoor LED module draws heavy direct current along its 5V power rails.
Layer Count: Commercial indoor modules must use a 4-layer PCB. This separates DC power planes and ground planes from high-frequency clock and data traces, eliminating electromagnetic interference and image ghosting. Cheap modules cut corners with a 2-layer board, running power and data side-by-side, which causes line jitter and localized thermal hot spots.
Substrate Thickness & Tg: Specify 1.6mm thickness with a glass transition temperature rating of TG150 or TG170. Flimsy 1.0mm or 1.2mm boards warp easily when heated, breaking the seamless alignment of adjacent panels.
Copper Foil Weight: Insist on minimum 1.5oz (52μm) copper foil. Thin 0.5oz copper traces generate high electrical resistance, causing severe voltage drops across the module that make center pixels visibly dimmer and redder than edge pixels.
When evaluating factory quotes, use this matrix to decode component specifications and verify where your money is actually going:
| Subsystem Component | Tier 1: Commercial / Broadcast Grade | Tier 2: Standard Commercial Grade | Tier 3: Budget / High Risk |
|---|---|---|---|
| LED Packaging | Nationstar Gold Wire / Nichia / Kinglight High-Bin | Kinglight Copper Wire / MLS (Mulinsen) | Unbranded white-box, alloy bond wire |
| Encapsulation Style | Flip-Chip COB / Vacuum GOB / Matte SMD | Standard SMD (Black Face / White Face) | Bare exposed SMD (Recycled dies) |
| Driver Silicon | Macroblock MBI5153 / Chipone ICN2153 (PWM) | Chipone ICN2038S / Silan Micro | Generic 74HC595 shift registers |
| PCB Construction | 1.6mm 4-Layer FR-4, TG170, ≥1.5oz Copper | 1.6mm 2-Layer FR-4, TG140, 1.0oz Copper | 1.2mm 2-Layer Composite, 0.5oz Copper |
| Scan Mode Ratio | 1/16 or 1/32 Scan Rate (Cooler running) | 1/32 or 1/40 Scan Rate | 1/40 to 1/64 Scan (Overdriven Current) |
| Native Refresh Rate | 3,840Hz – 7,680Hz (Zero Camera Flicker) | 1,920Hz | 960Hz – 1,200Hz (Severe Rolling Lines) |
| Power Terminals | Gold-Plated Phosphor Bronze VH4 Posts | Tin-Plated Brass Screw Terminals | Thin Steel-Plated Pins (Prone to Arcing) |
| Cabinet Chassis | Die-Cast Aluminum/Magnesium CNC (±0.05mm) | Die-Cast Standard Aluminum (±0.15mm) | Welded sheet-metal iron box (±0.5mm) |
A common procurement mistake is over-specifying pixel pitch. Buying a P1.2 display for a space where viewers sit ten meters away wastes capital budget that should have gone toward structural rigging, redundant power supplies, or certified video processing.
Let's look down below together at the practical operational parameters across common indoor pixel pitches:
| Pixel Pitch | Pixel Density (Dots / m²) | Minimum Viewing Distance | Maximum Indoor Output | Typical Ingress Protection | Primary Application Venue |
|---|---|---|---|---|---|
| P0.9 – P1.2 | 694,444 – 1,000,000 | 1.0m to 1.5m (~3 to 5 ft) | 600 – 800 nits | IP50 (Front COB) / IP20 (Rear) | Mission-critical control rooms, broadcast studios, executive suites |
| P1.5 – P1.8 | 308,641 – 444,444 | 1.5m to 2.5m (~5 to 8 ft) | 600 – 1,000 nits | IP40 (Front GOB) / IP20 (Rear) | Corporate lobbies, high-end retail flagships, university lecture halls |
| P2.0 – P2.5 | 160,000 – 250,000 | 2.0m to 3.0m (~6.5 to 10 ft) | 800 – 1,200 nits | IP30 (Front SMD) / IP20 (Rear) | Church sanctuaries, sports lounges, corporate auditoriums |
| P3.0 – P4.0 | 62,500 – 111,111 | 3.0m to 5.0m (~10 to 16 ft) | 800 – 1,500 nits | IP30 (Front SMD) / IP20 (Rear) | Large event halls, exhibit centers, high-hung concourse screens |
Before signing a purchase order or wiring a commercial deposit, work through these three pivotal technical dilemmas with your engineering team:
Because LED packaging houses sort semiconductor dies into strict optical and electrical bins, and wafer characteristics naturally drift across manufacturing runs.
Packaging facilities bin finished diodes according to three variables:
Dominant Wavelength (nm): Determines the exact hue of red, green, and blue.
Luminous Intensity (mcd): Determines brightness under a calibrated current.
Forward Voltage (Vf): Dictates electrical current consumption.
If you purchase replacement modules twelve months later, the green wavelength might drift from 525.0nm to 527.5nm. While that sounds tiny, the human eye easily detects a 1nm difference when two panels sit side-by-side displaying pure white.
Initial Production Run (Wavelength: 525.0nm) --> [ Seamless Neutral White ]
Later Batch Addition   (Wavelength: 527.5nm) --> [ Distracting Yellow-Green Patch ]
What should you do then?
Contractually mandate an upfront spare parts allowance of at least 5% to 8% fully assembled modules drawn directly from the same single-bin diode wafer lot.
Mandate receiving cards that support onboard calibration storage (such as Novastar Armor or A-series cards). This stores the sub-pixel chroma and luminance calibration coefficients directly on the module's EEPROM, allowing new panels to adapt to the surrounding wall automatically.
Yes, if thermal management, air conditioning loads, and diode lifespan matter.
In traditional Common Anode architecture, a single 5.0V DC power rail feeds the red, green, and blue diodes simultaneously.
Red diodes only require approximately 2.1V forward voltage to operate, while blue and green diodes require roughly 3.2V.
The excess 2.9V fed to the red diode is dissipated directly into the circuit board as pure waste heat through internal dropping resistors.
The board runs hot (often reaching 55°C to 65°C), accelerating diode degradation and putting extra strain on room HVAC systems.
In Common Cathode architecture, dual independent power rails feed the display:
A dedicated 2.8V rail powers the red diodes.
A separate 3.8V rail powers the green and blue diodes.
Power waste drops dramatically, lowering overall screen energy consumption by 25% to 35% and keeping cabinet temperatures 10°C to 15°C cooler. This cooler operating profile prevents color drifting and extends the operational half-life of the display.
Common Anode Architecture (Wasteful):
Single 5.0V Rail =====> [Red Diode (~2.1V)]  --> 2.9V Dissipated as Pure Heat!
                 =====> [Green Diode (~3.2V)]--> 1.8V Dissipated as Heat
                 =====> [Blue Diode (~3.2V)] --> 1.8V Dissipated as Heat

Common Cathode Architecture (Energy Efficient):
Dedicated 2.8V Rail --> [Red Diode (~2.1V)]  --> Only 0.7V Headroom (Runs Cool)
Dedicated 3.8V Rail --> [Green & Blue Diodes]--> Only 0.6V Headroom (Runs Cool)
Indoor modules draw significant direct current along the 5V power bus when displaying pure white at peak output.
If internal DC power wiring uses undersized copper or loose screw terminal blocks, the voltage will drop from 5.0V at the power supply terminal down to 4.4V or lower by the time it reaches the end of the module chain.
Red diodes have a lower forward voltage threshold (~1.9V to 2.1V) compared to blue and green diodes (~2.9V to 3.2V). When line voltage drops significantly, blue and green channels starve for headroom first, leaving corner pixels with a noticeable pink or reddish tint.
Require the factory to supply pure copper UL1015 14AWG or 16AWG DC power leads and route power in a star configuration rather than daisy-chaining more than two modules together. That way you can maintain clean voltage uniformity across every corner of the display.
Never release final progress payments or sign ocean bills of lading based on polished marketing photos sent over chat apps. Here is the exact five-step quality testing sequence our technicians use when auditing production runs in Shenzhen:
+---------------------------------------------------------------+
|               Pre-Shipment Factory Audit Sequence             |
+---------------------------------------------------------------+
| Step 1: Solder Joint & PCB Teardown Inspection                |
| Step 2: Seam Alignment & Mechanical Tolerance Verification    |
| Step 3: Low-Brightness Grayscale Linearity & D65 Calibration  |
| Step 4: 72-Hour Continuous Dynamic Burn-In & Thermal Scan     |
| Step 5: High-Voltage Dielectric Withstand & Ground Continuity |
+---------------------------------------------------------------+
Use an electric screwdriver to unfasten the front plastic mask from three randomly chosen sample modules.
Inspect the surface-mount solder fillets under a 20x jeweler's loupe. Solder joints around the SMD diode pads and driver IC leads must be smooth, shiny, and concave, fully covering the pads (conforming to IPC-A-610 Class 2 standards). Look out for dull, grainy finishes, cold solder joints, or solder whiskers between closely spaced IC pins.
Check the board edge: verified boards show distinct, crisp copper layering with clean FR-4 substrate cores. If the board edges look ragged or exhibit dark, fibrous cardboard-like layering, it is a sub-standard composite substrate.
Have factory technicians assemble a 3×3 cabinet array on a leveled precision granite inspection table.
Run your fingertips across the horizontal and vertical seams between adjacent cabinets. The surface transition should feel completely smooth, with seam gaps measuring less than 0.05mm.
If you can catch your fingernail on the edge of a module or slide a standard 0.2mm automotive feeler gauge between cabinets, the cabinet CNC milling was poorly calibrated and the wall will show visible black lines once mounted.
Indoor displays rarely run at 100% brightness; in an office or retail environment, they typically operate between 20% and 40% output to prevent eye fatigue.
Dim the display down to 15% brightness and inspect a 16-step gray ramp test pattern.
Look for grayscale banding, pink color tinting in dark grays, or flickering in the lowest steps. High-performance driver ICs maintain smooth, neutral-gray transitions even at very low output levels.
Position a colorimeter (such as a Klein K10-A) perpendicular to the screen center and verify that the white point achieves an exact D65 standard (CIE 1931: x = 0.3127, y = 0.3290) with luminance variance across the screen below 2%.
Demand a documented 72-hour burn-in process on the factory testing wall:
First 24 Hours: Cycle through pure primary colors (Red, Green, Blue) at maximum brightness to trigger infant mortality in marginal diodes.
Second 24 Hours: Run continuous 100% full-white balance to stress the power distribution traces and driver IC thermal dissipation vias.
Final 24 Hours: Play high-dynamic-range video loops with rapid black-to-white contrast shifts to test signal buffering and refresh stability.
Scan the active display wall with a handheld FLIR thermal camera. Look for abnormal thermal signatures. In a standard 25°C ambient room, a well-engineered module running full white should stay between 38°C and 48°C across the board. If individual driver ICs glow bright red past 65°C, it points to unbalanced power traces or poor thermal grounding.
Apply a dielectric withstand tester (Hi-Pot test) at 1,500V AC between the primary AC line inputs and the structural aluminum chassis for 60 seconds. Leakage current must remain strictly under 5mA.
Verify that ground path resistance between any exterior metal point and the main ground lug measures less than 0.1 ohms.
When your field service technicians are troubleshooting an active indoor LED display on site, use this root-cause diagnostic matrix to identify and isolate issues:
| Observed Symptom | Probable Root Cause | Corrective Field Action |
|---|---|---|
| A single horizontal band of 8 or 16 rows completely black | Blown output pin on the line-decoder IC (e.g., 74HC138) or damaged P-channel MOSFET switch (4953) | Replace the failed 4953 dual MOSFET or 74HC138 decoder chip on the rear of the module using a hot-air rework tool. |
| A single pixel stuck on pure Red, Green, or Blue | Internal semiconductor junction punch-through caused by electrostatic discharge (ESD) or solder whisker | De-solder and replace the individual SMD lamp bead using low-temperature solder paste (138°C bismuth alloy). |
| An entire 320×160mm module is completely dark | Blown 5V DC power fuse, loose power wiring harness, or failed buffer IC (74HC245) on data input | Verify 5.0V at terminal posts with a multimeter; check the 16-pin ribbon cable for oxidation; swap the input 74HC245 buffer. |
| Display shows high-frequency rolling lines on mobile cameras | Low PWM refresh rate configuration or excessive voltage drop below 4.5V | Verify power supply rail output under load; reconfigure the receiving card firmware to maximize refresh rate registers. |
| Corner pixels visibly dim and tinted pinkish-red | Heavy DC voltage drop along the power cable run, starving green and blue diodes of forward headroom | Measure DC bus voltage under full white; upgrade power injection cables from 16AWG to 14AWG pure copper runs. |
| Adjacent modules show dark seam lines under overhead room lighting | Mounting magnets seated unevenly or cabinet frame out of planar tolerance | Adjust the six-axis magnetic adjustment screws on the rear of the module using an Allen wrench to level the module face. |
A video wall is only as stable as the electrical infrastructure supporting it behind the scenes:
Never pair high-spec modules with generic, unbranded power supplies:
Standardize on recognized industrial units like Mean Well (specifically the fanless, slimline UHP-200-5 or LRS-350-5 series) or certified commercial equivalents from Great Wall.
Calculate your power requirements so the power supplies run at no more than 70% to 75% of their rated continuous load. Running power supplies at maximum capacity generates excessive heat, shortens internal capacitor lifespans, and introduces electrical noise onto the 5V rails, which shows up as subtle horizontal jitter on the screen.
Cabinet Power Calculation Rule:
Total Module Peak Watts = (Module Count x Max Draw)
Required Power Supply Rating = Total Module Peak Watts / 0.70
Rely on established control platforms like Novastar (such as their TB-series multimedia players for standalone displays or COEX/VX-series processors for live multi-source video walls) or Colorlight.
Use shielded CAT6 network cabling with high-quality RJ45 connectors for internal cabinet data loops to prevent electromagnetic interference from nearby building systems.
When you spend years managing visual infrastructure across demanding installations, practical engineering reality always supersedes sales marketing.
Avoid getting dragged into meaningless specification wars. A factory promising 1,500 nits on an indoor P2.5 display is not offering advanced technology; they are simply pushing standard diodes with excessive forward current. In a normal commercial interior, running an LED screen at 1,500 nits causes immediate eye strain for anyone sitting nearby. A calibrated, stable 600 to 800 nits running on a conservative duty cycle with high optical contrast and a deep black resin face is vastly better for day-to-day readability and will outlast an overdriven screen every single time.
Make sure your purchase contract explicitly names every critical component model down to the part number. Never accept vague phrasing like "Nationstar or equivalent" or "high-refresh Taiwan driver IC." Your purchase order should clearly specify: Nationstar Copper-Wire SMD (or Flip-Chip COB), Macroblock MBI5153 Driver IC, 1.6mm 4-Layer TG170 FR-4 PCB, Common Cathode (if specified), and Mean Well UHP Power Supplies. Having exact component specifications on paper gives you contractual protection if substitutions occur during production.
Finally, protect your investment by keeping spare parts on hand from day one. For an installation of 200 modules, always mandate an initial spare package containing at least 15 complete, factory-burned-in modules drawn from the exact same diode wafer and color-binning run, 1,000 loose matching LEDs on tape-and-reel, 50 driver ICs, two spare receiver cards, and plenty of spare ribbon cables and power leads. Having exact-match replacement parts stored locally in your warehouse prevents costly display downtime and ensures that any future maintenance seamlessly matches your screen’s original color temperature and brightness profile.
Hope this hands-on breakdown helps you dodge common supply chain traps and build rock-solid full color video walls that deliver flawless visual performance for years to come.
Working directly with audited OEM/ODM factories allows commercial integrators to bypass 30% to 50% distributor markups, customize cabinet dimensions and magnetic mounting points to exact architectural drawings, lock in single-bin diode lots for uniform color temperature, and specify component-level BOM standards (such as gold bond wires, TG170 4-layer PCBs, and Mean Well power supplies) that wholesale brokers cannot guarantee.
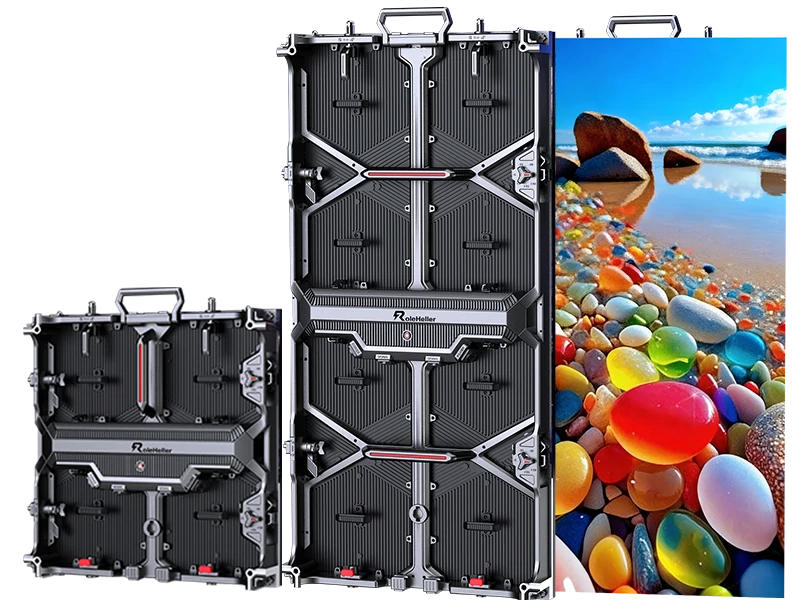
The global commercial standard for indoor LED modules is 320mm × 160mm. This size holds standard aspect ratios and cleanly mounts into 640mm × 480mm die-cast aluminum cabinets in a 2×3 configuration, making it straightforward to construct standard 16:9 widescreen video walls matching native 1080p, 4K, and 8K resolutions. Another common format for square rental cabinets is 250mm × 250mm (used in 500mm × 500mm frames).
Tier-1 commercial manufacturers primarily specify Nationstar (particularly their black-body copper-wire and gold-wire commercial lines) and Kinglight. Secondary commercial options include Honglitronic and Mulinsen (MLS). For ultra-premium broadcast or virtual production spaces, Japanese Nichia LEDs are specified. Generic, unbranded white-box diodes should be avoided for permanent installations due to inconsistent color binning and high early failure rates.
SMD (Surface Mount Device) solders individual lamp beads to the board surface, offering good color accuracy and lower cost, but leaving diodes vulnerable to physical impact. GOB (Glue-on-Board) adds an optically clear polyurethane coating over standard SMD boards, protecting diodes from collision, dust, and moisture. COB (Chip-on-Board) bonds bare semiconductor dies directly to the PCB substrate without lead frames, encased under optical resin, delivering higher contrast, extreme impact resistance, and an ultra-low pixel failure rate (<5 PPM).
Price differences reflect the underlying bill of materials. An inexpensive panel typically uses a 2-layer composite PCB, generic shift registers without PWM, copper-alloy wire diodes, manual silicone potting, and basic sheet-metal cabinets without anti-rust primer. A commercial-grade display uses a 4-layer TG170 fiberglass PCB with 1.5oz copper, branded Macroblock PWM driver ICs, gold-wire LEDs, automated polyurethane potting, and CNC-machined die-cast aluminum cabinets.
Yes, provided you specify front-service modules and compatible cabinets. Indoor modules feature precision magnetic mounting pillars that attach securely to the steel or aluminum cabinet frame. Technicians can remove individual modules in under ten seconds using a handheld vacuum suction tool directly from the front face, allowing video walls to be mounted flush against walls without requiring a rear service corridor.
Common Anode powers red, green, and blue diodes from a single 5V DC rail, dissipating significant excess voltage on the red diode (~2.1V required) as pure waste heat. Common Cathode utilizes dual independent power rails (typically 2.8V for red and 3.8V for green/blue), which slashes energy consumption by 25% to 35%, lowers operating temperatures by 10°C to 15°C, prevents color shifting, and extends the operational lifespan of the diodes.
Schedule an unscheduled live video audit during regular working hours in Shenzhen or Huizhou. Mandate a continuous walkthrough showing their automated SMT surface-mount lines (checking for equipment from brands like Yamaha or Panasonic), automated optical inspection (AOI) benches, robotic conformal coating lines, and an active 72-hour burn-in testing wall. Trading intermediaries will usually deflect, provide pre-recorded promotional videos, or show only sales offices and commercial showrooms.
Specify a native refresh rate of at least 3,840Hz powered by dedicated PWM constant-current driver ICs. For virtual production (XR stages), broadcast television studios, or conference rooms where video conferencing cameras are deployed, specify ultra-high refresh driver silicon capable of 7,680Hz with low scan rates to eliminate rolling black scan lines, moiré artifacts, and high-frequency camera banding.
For North American installations, specify FCC Part 15 Class A/B for electromagnetic compatibility, along with complete cabinet-level safety certifications to UL 48 / UL 8750 or ETL equivalent, with internal power supplies certified to UL 62368-1. For European installations, require third-party accredited lab test reports for CE-EMC (EN 55032/EN 55035), CE-LVD (EN 62368-1), and full RoHS compliance covering hazardous substance restrictions.