English
If you need an immediate, field-tested answer on choosing 8K LED display manufacturers without getting burned by marketing hype or five-figure service bills, here is the direct benchmark: partner strictly with established display engineering manufacturers that utilize flip-chip Chip-on-Board (COB) or Micro-LED in Package (MIP) technology with true common-cathode driver architecture, paired with native 8K broadcast-grade processing platforms like Megapixel VR Helios, NovaStar COEX (such as the CX80 Pro or dual MX40 Pro setups), or Brompton Technology. For turnkey enterprise boardrooms, virtual production volume stages, and mission-critical command centers, the manufacturers with proven track records are Planar/Leyard, SiliconCore Technology, Unilumin, Absen, and Sony (Crystal LED). If a supplier tries to sell you traditional surface-mount SMD 1010 diodes for an 8K canvas, cannot prove point-to-point uncompressed pixel mapping over HDMI 2.1 or SMPTE ST 2110, or fails to provide third-party thermal imaging reports from a continuous 72-hour burn-in run, pass on them immediately—no matter how cheap their proposal looks.
Have you ever sat in an executive briefing room or broadcast control suite, looked at a supposedly cutting-edge video wall, and immediately spotted faint grid seams, blurry text scaling, or heat radiating off the screen like a radiator? When we are using ultra-high-resolution displays in enterprise environments, stepping up to native 8K—which means a massive 7680 × 4320 canvas packing 33.17 million active pixels—leaves zero margin for manufacturing sloppiness. At pixel pitches between 0.4 mm and 0.9 mm, a placement tolerance error of just ten micrometers creates glaring visual gaps. Yet when you search for 8K LED display manufacturers, you get hit with dozens of conflicting proposals ranging from $90,000 to over $600,000. Some vendors promise "8K resolution" but are secretly using hardware scalers on a 4K physical surface, while others deliver displays that pull so much power they require an industrial chiller just to keep the room habitable. What should you do then? You end up paying twice as much to fix structural and cooling problems that should have been caught in the design phase. Let's dive in and unpack the actual engineering realities, manufacturer tiers, and factory auditing protocols you need to know.
To evaluate 8K hardware properly, you have to discard standard consumer television thinking. In consumer electronics, an 8K TV packs 33 million pixels onto an 85-inch glass panel using liquid crystal or OLED sheets. With direct-view LED, however, the display is built by hand-assembling hundreds of modular cabinet tiles.
The physical dimensions of an 8K LED wall depend strictly on the pixel pitch (center-to-center diode spacing):
[Pixel Pitch vs. Physical Screen Dimensions for Native 8K (7680 × 4320)]
P0.4 mm  ──► Width: 3.07 m (10.1 ft)  ×  Height: 1.73 m (5.7 ft)  ──► Diagonal: 139 in
P0.6 mm  ──► Width: 4.61 m (15.1 ft)  ×  Height: 2.59 m (8.5 ft)  ──► Diagonal: 208 in
P0.78 mm ──► Width: 6.00 m (19.7 ft)  ×  Height: 3.37 m (11.1 ft) ──► Diagonal: 271 in
P0.93 mm ──► Width: 7.20 m (23.6 ft)  ×  Height: 4.05 m (13.3 ft) ──► Diagonal: 325 in
P1.25 mm ──► Width: 9.60 m (31.5 ft)  ×  Height: 5.40 m (17.7 ft) ──► Diagonal: 434 in
Notice the practical takeaway: if a vendor tries to quote you P1.25 mm modules for an executive boardroom that only has an eight-foot ceiling, that wall cannot physically display native 8K without spilling into the floor and ceiling slabs. To fit an 8K display into a standard corporate boardroom or luxury residential media room with typical nine-to-ten-foot ceilings, you are practically forced into the sub-0.8 mm arena (P0.6 mm to P0.78 mm).
At these microscopic pitches, the minimum viewing distance drops below 1.2 meters (roughly 4 feet). Viewers can stand arm's-length from the wall and review detailed CAD schematics, geological seismic maps, or live financial trading feeds with zero visible pixel structure. But packing 33 million light-emitting elements onto a wall creates immense thermal and mechanical challenges that traditional LED displays never had to solve.
When reviewing quotes from various 8K LED display manufacturers, the packaging method is the single biggest factor governing visual contrast, durability, and failure rates over time.
[Traditional SMD 0808/1010]           [Flip-Chip COB]                    [Micro-LED in Package (MIP)]
┌─────────────────────────┐         ┌─────────────────────────┐        ┌─────────────────────────┐
│ Exposed pins & wire weld│         │ Integrated resin layer  │        │ Micro-die on mini-carrier│
│ Vulnerable to physical  │         │ Bare flip-chip on board │        │ Discrete testing before  │
│ impact and humidity     │         │ High black contrast     │        │ placement on substrate   │
└─────────────────────────┘         └─────────────────────────┘        └─────────────────────────┘
Standard surface-mount devices (SMD 0808 or SMD 1010) use miniature plastic housings containing three color chips bonded with micro-wires to external metal pins.
At pitches below 1.0 mm, the solder pads become so microscopic that surface tension during reflow soldering causes high defect rates.
The diodes sit raised above the circuit board surface without physical shielding. If an installer's sleeve or an office cleaning cloth catches the corner of a tile, it will shear several diodes clean off the board.
Exposed copper pins are vulnerable to moisture-induced oxidation and silver migration, leading to dead sub-pixels within 12 to 18 months.
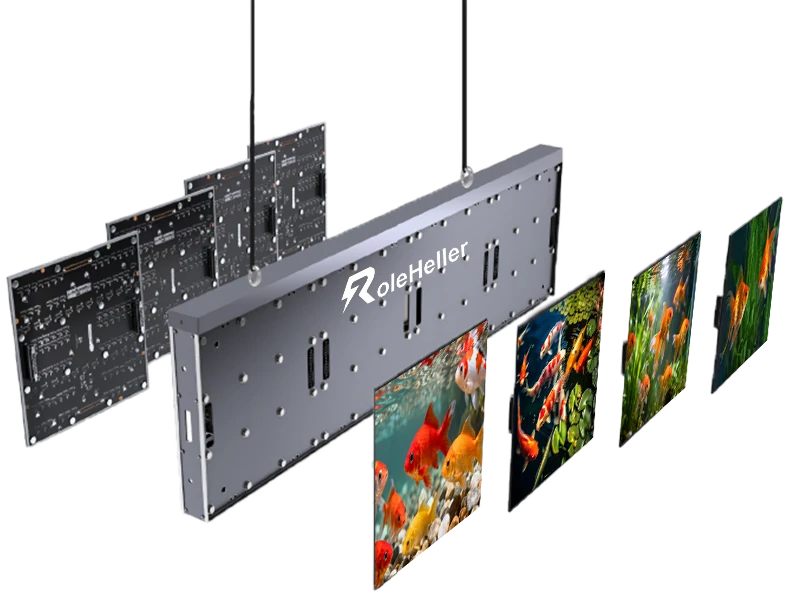
In flip-chip COB, bare microscopic LED semiconductor dies are mounted directly onto the printed circuit board face-down, eliminating bonding wires entirely. The entire surface is then sealed under an optical-grade epoxy or polyurethane resin matrix.
The Good: Unmatched black levels and contrast ratios exceeding 20,000:1. The smooth, flat resin surface provides an IP54 or IP65 front barrier against dust, moisture, and physical impact. You can run your hand across it without knocking off pixels. It also conducts heat away from the chips directly into the PCB substrate.
The Catch: If a micro-pixel fails inside a COB tile, on-site field repairs are impossible. You cannot touch it with a standard soldering iron; the entire module must be swapped out and shipped back to the factory for specialized laser de-bonding and cleanroom micro-rework.
MIP is an advanced packaging methodology developed to bridge the gap between COB performance and SMD repairability. Bare micro-LED chips (under 50 microns) are pre-packaged onto miniature carrier substrates (such as 0404 or 0202 packages), optically tested and binned at the packaging stage, and then placed onto the display PCB using high-speed SMT placement.
The Good: Because each MIP package is tested and color-binned before SMT placement, color uniformity across huge walls is remarkably consistent. Unlike COB, individual damaged MIP packages can be reworked on an integrator's service bench using precision micro-tweezers and hot-air tools.
The Catch: It carries a higher component packaging cost compared to mass-produced COB, making it a premium solution primarily used by high-end broadcast and creative studio manufacturers.
To help you benchmark proposals across the global manufacturing landscape, here is how the established players stack up across engineering architectures:
| Manufacturer / Brand | Core 8K Packaging Architecture | Native Pitch Range for 8K | Primary Processing Platform | Heat / Power Management | Best Commercial Use-Case |
|---|---|---|---|---|---|
| Sony (Crystal LED / C & B-Series) | Proprietary Micro-LED (Surface treated) | P0.78 mm – P1.25 mm | Sony ZRA-1 / ZRA-2 Image Processors | Conduction-cooled, low surface temp | Flagship corporate lobbies, high-end automotive design studios |
| SiliconCore Technology | Common-Cathode Fine-Pitch COB / ZACH | P0.63 mm – P1.2 mm | Custom FPGA with ZACH Driver Tech | Patented Common-Cathode (runs cool to touch) | Mission-critical command centers, simulation, high-lux boardrooms |
| Planar / Leyard (DirectLight Pro / V-Series) | Flip-Chip COB / CarbonLight Micro-LED | P0.6 mm – P0.9 mm | Planar WallDirector / Megapixel VR | Common-Cathode distributed power supplies | Government control rooms, broadcast newsrooms, luxury residential |
| Unilumin (UMicro / UMini Series) | Advanced Flip-Chip COB (54-inch panels) | P0.4 mm – P0.9 mm | NovaStar COEX / Megapixel VR Helios | High-density passive dissipation | Enterprise auditoriums, command centers, visual monitoring hubs |
| Absen (Clear Cobalt / Micro Series) | Black-Coating COB / MIP Hybrid | P0.7 mm – P0.9 mm | NovaStar COEX / Brompton Tessera | Surface-cooling dynamic drive | High-end conference facilities, virtual production studios |
| Infiled (WP Series / Apex Series) | Ultra-Thin COB / Fine-Pitch Modular | P0.9 mm – P1.2 mm | NovaStar / Colorlight Pro | High-efficiency aluminum chassis | Corporate briefing centers, sports control rooms |
When we are installing an 8K wall consisting of thirty million diodes running in an enclosed space, heat is your biggest operational enemy. In a standard common-anode circuit, a single 4.2V or 5V power bus feeds the red, green, and blue semiconductor dies simultaneously.
The electrical physics breakdown:
Blue and green LED dies need roughly 2.8V to 3.1V of forward voltage to emit light.
Red LED dies require only 1.8V to 2.1V.
In a common-anode circuit, that extra 1.0V to 1.3V pumped into the red diode does not produce more lumens; it gets converted directly into thermal waste inside the driver chip and diode junction.
Multiply that waste by thirty-three million sub-pixels, and a common-anode 8K wall can dump 12 to 18 kilowatts of radiant heat into a conference room. The front surface of the screen will heat up to 55°C (131°F), cooking the internal solder points, causing color drift across hot spots, and forcing the facility team to over-engineer the building's HVAC ducting.
[Common Anode: High Heat Waste]
Power Rail (5.0V) ──► Red Diode (Draws 2.0V)  ──► 3.0V Wasted as Pure Heat!
                  ──► Green Diode (Draws 3.0V) ──► 2.0V Wasted
                  ──► Blue Diode (Draws 3.0V)  ──► 2.0V Wasted

[Common Cathode: Energy Efficient & Cool]
Rail A (1.8V - 2.0V) ──► Red Diode   ──► Negligible Thermal Waste
Rail B (2.8V - 3.0V) ──► Green Diode ──► Low Heat
Rail C (2.8V - 3.0V) ──► Blue Diode  ──► Low Heat
This is why top-tier 8K manufacturers mandate Common-Cathode architecture. By separating the electrical rails—feeding an independent 1.8V to red and 2.8V to blue and green—overall panel power consumption drops by 25% to 38%. The front display surface stays between 32°C and 36°C (barely above ambient skin temperature). That way, executives or talent standing right in front of the screen will never feel a wall of heat radiating into their faces.
Building a physical 8K LED display is only half the battle. Getting a pristine 8K uncompressed video stream from your media servers onto the screen requires an enormous data pipeline.
Consider the raw throughput numbers:
An uncompressed 8K signal (7680 × 4320) running at 60 Hz with 10-bit color depth (4:4:4 chroma sampling) requires approximately 48 Gbps of uncompressed bandwidth.
If you step up to 120 Hz for high-frame-rate broadcast or simulation, that requirement doubles to nearly 96 Gbps.
[Master 8K Media Server / Graphics Engine]
                    │
                    ▼ (HDMI 2.1 / Dual DP 1.4 / 100GbE SMPTE ST 2110)
[Enterprise 8K Display Processor (e.g., Megapixel VR Helios / NovaStar CX80 Pro)]
                    │
                    ├─ Multi-10G / 25G Fiber Trunk A (Main Canvas Left)
                    └─ Multi-10G / 25G Fiber Trunk B (Main Canvas Right)
                    │
                    ▼
[Cabinet Receiving Cards with Frame-Lock & Genlock Synchronization]
When reviewing manufacturer processing packages, verify the following signal pipeline details:
True Native Inputs: The controller must accept native single-cable HDMI 2.1 (Fixed Rate Link at 48 Gbps) or dual DisplayPort 1.4/2.0 inputs. Avoid systems that require you to split an 8K video into four separate 4K HDMI 2.0 cables using external quadrant scalers; quad-cable setups introduce frame synchronization jitter and micro-tearing across quadrant boundary seams.
Genlock and Frame-Locking: For broadcast studios and virtual production stages, all processing cards and receiver units must support hardware Genlock (Blackburst or Tri-Level sync). Without frame-locked genlock, broadcast cameras shooting the video wall will capture subtle rolling horizontal artifacts.
Low Latency Pipeline: If the screen is used for interactive simulations or live corporate videoconferencing, total processing latency from input port to LED emission must remain under 1 frame (less than 16 milliseconds at 60 Hz). Processors like the Megapixel VR Helios or Brompton Tessera accomplish this with sub-frame processing, whereas budget domestic processors often introduce 3 to 4 frames of latency, making live mouse cursor tracking or interactive telepresence feel completely sluggish.
To help you understand where costs diverge when sourcing from 8K manufacturers, examine the hardware configuration tiers below:
| Technical Spec | Commercial Enterprise Spec | Mission-Critical Command Spec | Ultra-Luxury & Broadcast Spec |
|---|---|---|---|
| Wholesale Price Range (Complete Wall) | $3,500 – $5,500 / m² | $6,000 – $9,500 / m² | $12,000 – $22,000+ / m² |
| Pixel Pitch Range | P0.78 mm – P0.93 mm | P0.6 mm – P0.78 mm | P0.4 mm – P0.6 mm |
| Packaging Architecture | Flip-Chip COB (Matte Black) | Common-Cathode COB / MIP | Proprietary Micro-LED / Optical Layer |
| Luminance Output | 600 – 800 Nits (Calibrated) | 800 – 1,200 Nits (Adjustable) | 1,000 – 1,800 Nits (HDR10 / HLG) |
| Contrast Ratio | 10,000:1 | 20,000:1 | 1,000,000:1 (Infinite black) |
| Refresh Rate | 3,840 Hz | 3,840 Hz – 7,680 Hz | 7,680 Hz Low-Latency Frame Sync |
| Grayscale Depth | 14-bit to 16-bit | 16-bit to 18-bit Low-Gray Clear | 16-bit to 22-bit True Color Depth |
| Chassis Tolerance | CNC Aluminum (±0.03 mm) | 5-Axis CNC Magnesium (±0.01 mm) | Aerospace Alloy Floating Mounts |
| Cooling Method | Passive Conduction / Fanless | Fanless Common-Cathode | Fanless Zero-Noise Conduction |
| Redundant Hardware | Dual power supplies | Dual power + Dual data loop | 100% N+1 Power & Hot-Swap Data |
At a pixel pitch of 0.6 mm, the distance between adjacent diodes is roughly the thickness of five sheets of copy paper. If two structural cabinets have a mechanical alignment error of just 0.05 mm (fifty micrometers), the gap between the modules will look like a dark, distracting seam cutting right through the middle of an image.
When inspecting cabinet hardware from 8K LED display manufacturers, look for these mechanical features:
5-Axis CNC Machined Chassis: The mating edges of the cabinets must be milled on high-precision 5-axis CNC machines after casting. Raw die-cast aluminum cools unevenly and shrinks; only secondary precision milling ensures that cabinet corners meet at exact 90-degree angles within a tolerance of ±0.01 mm.
Precision Locating Pins and Bushings: Cabinets must utilize hardened stainless steel tapered locator pins that seat into precision-bored brass or steel bushings on the mating cabinet. When cabinets are clamped together, these mechanical pins force the frames into exact planar alignment before locking bolts are engaged.
Z-Axis Planar Adjustment: Building walls are never flat. Drywall, concrete cores, and steel studs will always have slight surface waviness. The mounting sub-frame must feature independent, micro-threaded Z-axis adjustment points at every cabinet junction. Installers must be able to turn a fine hex-key screw to move a cabinet corner forward or backward by 0.1 mm increments until the entire display wall forms an optically flat plane without any tile lip or edge shadowing.
When investing hundreds of thousands of dollars in an 8K display, relying on slick brochures or pre-recorded showroom videos is a massive gamble. You should inspect the manufacturing plant personally or hire an accredited third-party engineering inspection firm to audit the production run.
[Cleanroom SMT & Die Placement (Class 1,000 / 10,000)]
                          │
                          ▼
[Automated 3D SPI Solder Paste & High-Precision Die Bonding]
                          │
                          ▼
[Multi-Zone Vacuum Reflow Oven & Automated Optical Inspection (AOI)]
                          │
                          ▼
[Optical Resin Potting & Surface Planar Measurement]
                          │
                          ▼
[Full-Raster 72-Hour Continuous White Burn-in Marathon]
                          │
                          ▼
[Calibrated Thermal Imaging & 33-Million Pixel Camera Calibration]
                          │
                          ▼
[Shock-Proof Wooden Crating with Moisture Vacuum Seals]
Narrow-pitch flip-chip COB and MIP manufacturing cannot take place in a standard electronics assembly shop. Microscopic airborne dust particles landing on a PCB pad before chip mounting will prevent proper electrical contact or create dark spots under the resin.
The die bonding and surface mounting cleanroom must be certified to ISO Class 7 (Class 10,000) or cleaner, with positive pressure airflow, sticky floor mats, and strict anti-static gowning protocols.
Diodes and semiconductor wafers must be transferred directly from climate-controlled dehumidification dry-cabinets into automated pick-and-place lines.
Because micro-LED dies have solder pads hidden entirely beneath the chip body, standard 2D optical cameras cannot verify solder integrity.
Demand to see the factory's automated 3D X-ray inspection station.
A random sampling of production boards must undergo X-ray scanning to verify that solder voiding beneath driver ICs and micro-dies is well under 10%, guaranteeing robust electrical and thermal pathways.
Early semiconductor failure follows the classic bathtub curve: if a driver IC or micro-die has an internal chemical defect or weak solder connection, it will fail within the first 48 to 72 hours of sustained electrical stress.
The manufacturer must assemble the complete 8K display wall in their testing bay and run it continuously for at least 72 uninterrupted hours before packing.
The cycle must include: 24 hours of full-raster white screen at 100% brightness (pushing power supplies and thermal dissipation to peak load), 24 hours of primary red, green, and blue patterns to expose stuck or drifting sub-pixels, and 24 hours of dynamic high-frame-rate video playback.
During the full-white burn-in test, walk the aging line with a calibrated thermal imaging camera. If any driver IC or power terminal spikes above 65°C in an ambient 25°C room, the thermal design is inadequate and those components will prematurely fail in field conditions.
Before crating the display, the manufacturer must run full-screen camera-based pixel-level calibration (chroma and luma calibration). A high-resolution CCD calibration camera captures the optical output of every single diode across the entire 8K canvas, calculates correcting coefficient matrices for red, green, and blue, and flashes those calibration values directly into the onboard EEPROM memory of each receiving card. This eliminates subtle batch color variances and ensures seamless edge blending across modular boundaries.
Question: Can I replace a damaged module on an 8K wall three years down the road without noticing a color mismatch?
Answer: Physically, the new tile will slot right into the cabinet, but optically, it will look like an off-color patch unless your spare parts were drawn from the exact same manufacturing wafer run. Semiconductor crystal growth yields natural variations in dominant wavelength and forward voltage between different production lots. That is why you must contractually require the manufacturer to provide a 5% to 8% single-bin spare parts package manufactured simultaneously with your main display wall. Store those batch-matched spares in an anti-static, climate-controlled cabinet on site so your technicians always have identical tiles ready to deploy.
Question: What happens if an 8K video wall loses power unexpectedly during a storm?
Answer: Powering up thirty-three million LEDs simultaneously creates an enormous electrical inrush current that can trip building circuit breakers or damage power supplies. Professional 8K display systems integrate intelligent sequential power-up sequencing. Rather than hitting the electrical grid all at once, internal relays stagger the power-up across cabinet columns in millisecond intervals. Additionally, enterprise controllers store full calibration and mapping files in non-volatile flash memory, meaning the screen restores its exact geometry and color profile automatically within seconds of power restoration.
Question: Front-service vs. rear-service—which mechanical design should I specify for an 8K installation?
Answer: You should specify 100% front-serviceable cabinets in virtually every corporate, broadcast, and luxury installation. Modern 8K walls are mounted flush against drywall, integrated into executive woodwork, or installed in tight control rooms where sacrificing two to three feet of floor space for a rear maintenance corridor is out of the question. Front-service modules attach via precision magnetic floating mounts. Using an electric vacuum extraction tool, a service technician can pull an individual module straight forward from the screen face in less than five seconds without touching adjacent tiles.
When you are ready to issue purchase orders and negotiate commercial contracts with 8K LED display manufacturers, keep these field-tested guidelines in mind:
First, never buy production quantities based on a small tabletop demo sample. A single 300 mm tile shown in a brightly lit exhibition booth tells you nothing about how a massive 30-foot wall will handle seam tolerances, thermal dissipation, or power supply hum. Always demand a live video inspection or on-site walkthrough of an assembled multi-cabinet array (at least 4K resolution) running full-raster white and dark video patterns before approving production.
Second, lock down your bill of materials (BOM) in your legally binding purchase agreement. Do not accept vague marketing phrases like "High-Definition Micro-LED Display." The purchase contract must specify:
Exact packaging architecture: Flip-Chip COB with matte-black anti-glare optical coating (or specified MIP package).
Diode specification: Custom single-bin micro-die with verified dominant wavelength tolerance within ±1.5 nm.
Driver IC model: Macroblock MBI5359 or custom common-cathode PWM driver with minimum 3,840 Hz refresh rate.
Cabinet construction: 5-Axis CNC machined aluminum/magnesium alloy, front-service magnetic extraction, verified seam tolerance within ±0.01 mm.
Power architecture: Common-Cathode distributed power supplies with active Power Factor Correction (PFC > 0.95).
Processing platform: Megapixel VR Helios or NovaStar COEX CX80 Pro with native HDMI 2.1 inputs and hardware Genlock support.
Third, structure your payment terms around verified factory acceptance milestones. The standard overseas trade term is a 30% deposit upon order confirmation, with the remaining 70% balance paid before dispatch. Never wire that final 70% based purely on factory-provided photos or prerecorded video clips. Hire an independent third-party engineering inspection agency to visit the factory floor, verify that the serial numbers match your specific production batch, audit the live 72-hour burn-in line, and supervise the crating process. That small inspection fee is the cheapest insurance policy you will ever buy.