English

Vetting dependable and technically certified glass led display manufacturers requires auditing five critical engineering thresholds before you even request a price quote: first, the factory must operate in-house Class 10,000 cleanroom autoclaves capable of high-pressure PVB or SGP structural glass lamination rather than relying on cheap cold-cure resin; second, the optical circuit design must utilize high-conductivity transparent conductive films (like patterned metal-mesh or high-grade ITO) yielding verifiable visual transmittance above 80% alongside calibrated brightness exceeding 5,000 nits for direct sunlit glass curtain walls; third, the supplier must provide traceable component-level binning reports from tier-one diode packagers (Nationstar, Kinglight, or Nichia); fourth, the assembled architectural glass must hold genuine, factory-owned safety and electrical certifications including ANSI Z97.1, EN 12150, UL 62368-1, UL 8750, and FCC Class B; fifth, the manufacturer must offer a documented modular service plan that explains exactly how pixel failures are addressed once glass panels are installed thirty floors above street level. If an overseas vendor fails to demonstrate these five capabilities on an unedited, live-streamed facility walkthrough within forty-eight hours, they are almost certainly an ordinary commercial display assembler subcontracting glass lamination to third-party glazers.
You have probably received a high-visibility architectural mandate: an international airport transit concourse, a high-end luxury retail flagship in Central, a commercial corporate atrium in Frankfurt, or a cultural museum facade in New York. You open your browser, enter "glass led display manufacturers" into the search bar, and get inundated with dozens of vendor catalogs showcasing dramatic 3D architectural renders. One supplier quotes $1,100 per square meter, another asks $4,600, and a third offers flexible adhesive film while calling it "structural LED glass." When you push their sales reps on technical realities—such as thermal expansion differences between soda-lime glass and epoxy substrates, solar heat gain coefficient (SHGC) impacts on your building HVAC system, or how to avoid micro-bubble delamination under sustained summer ultraviolet radiation—the conversation suddenly stalls. What should we do when custom architectural glass and active micro-electronics collide on a multi-million-dollar construction site? Let's dive in!
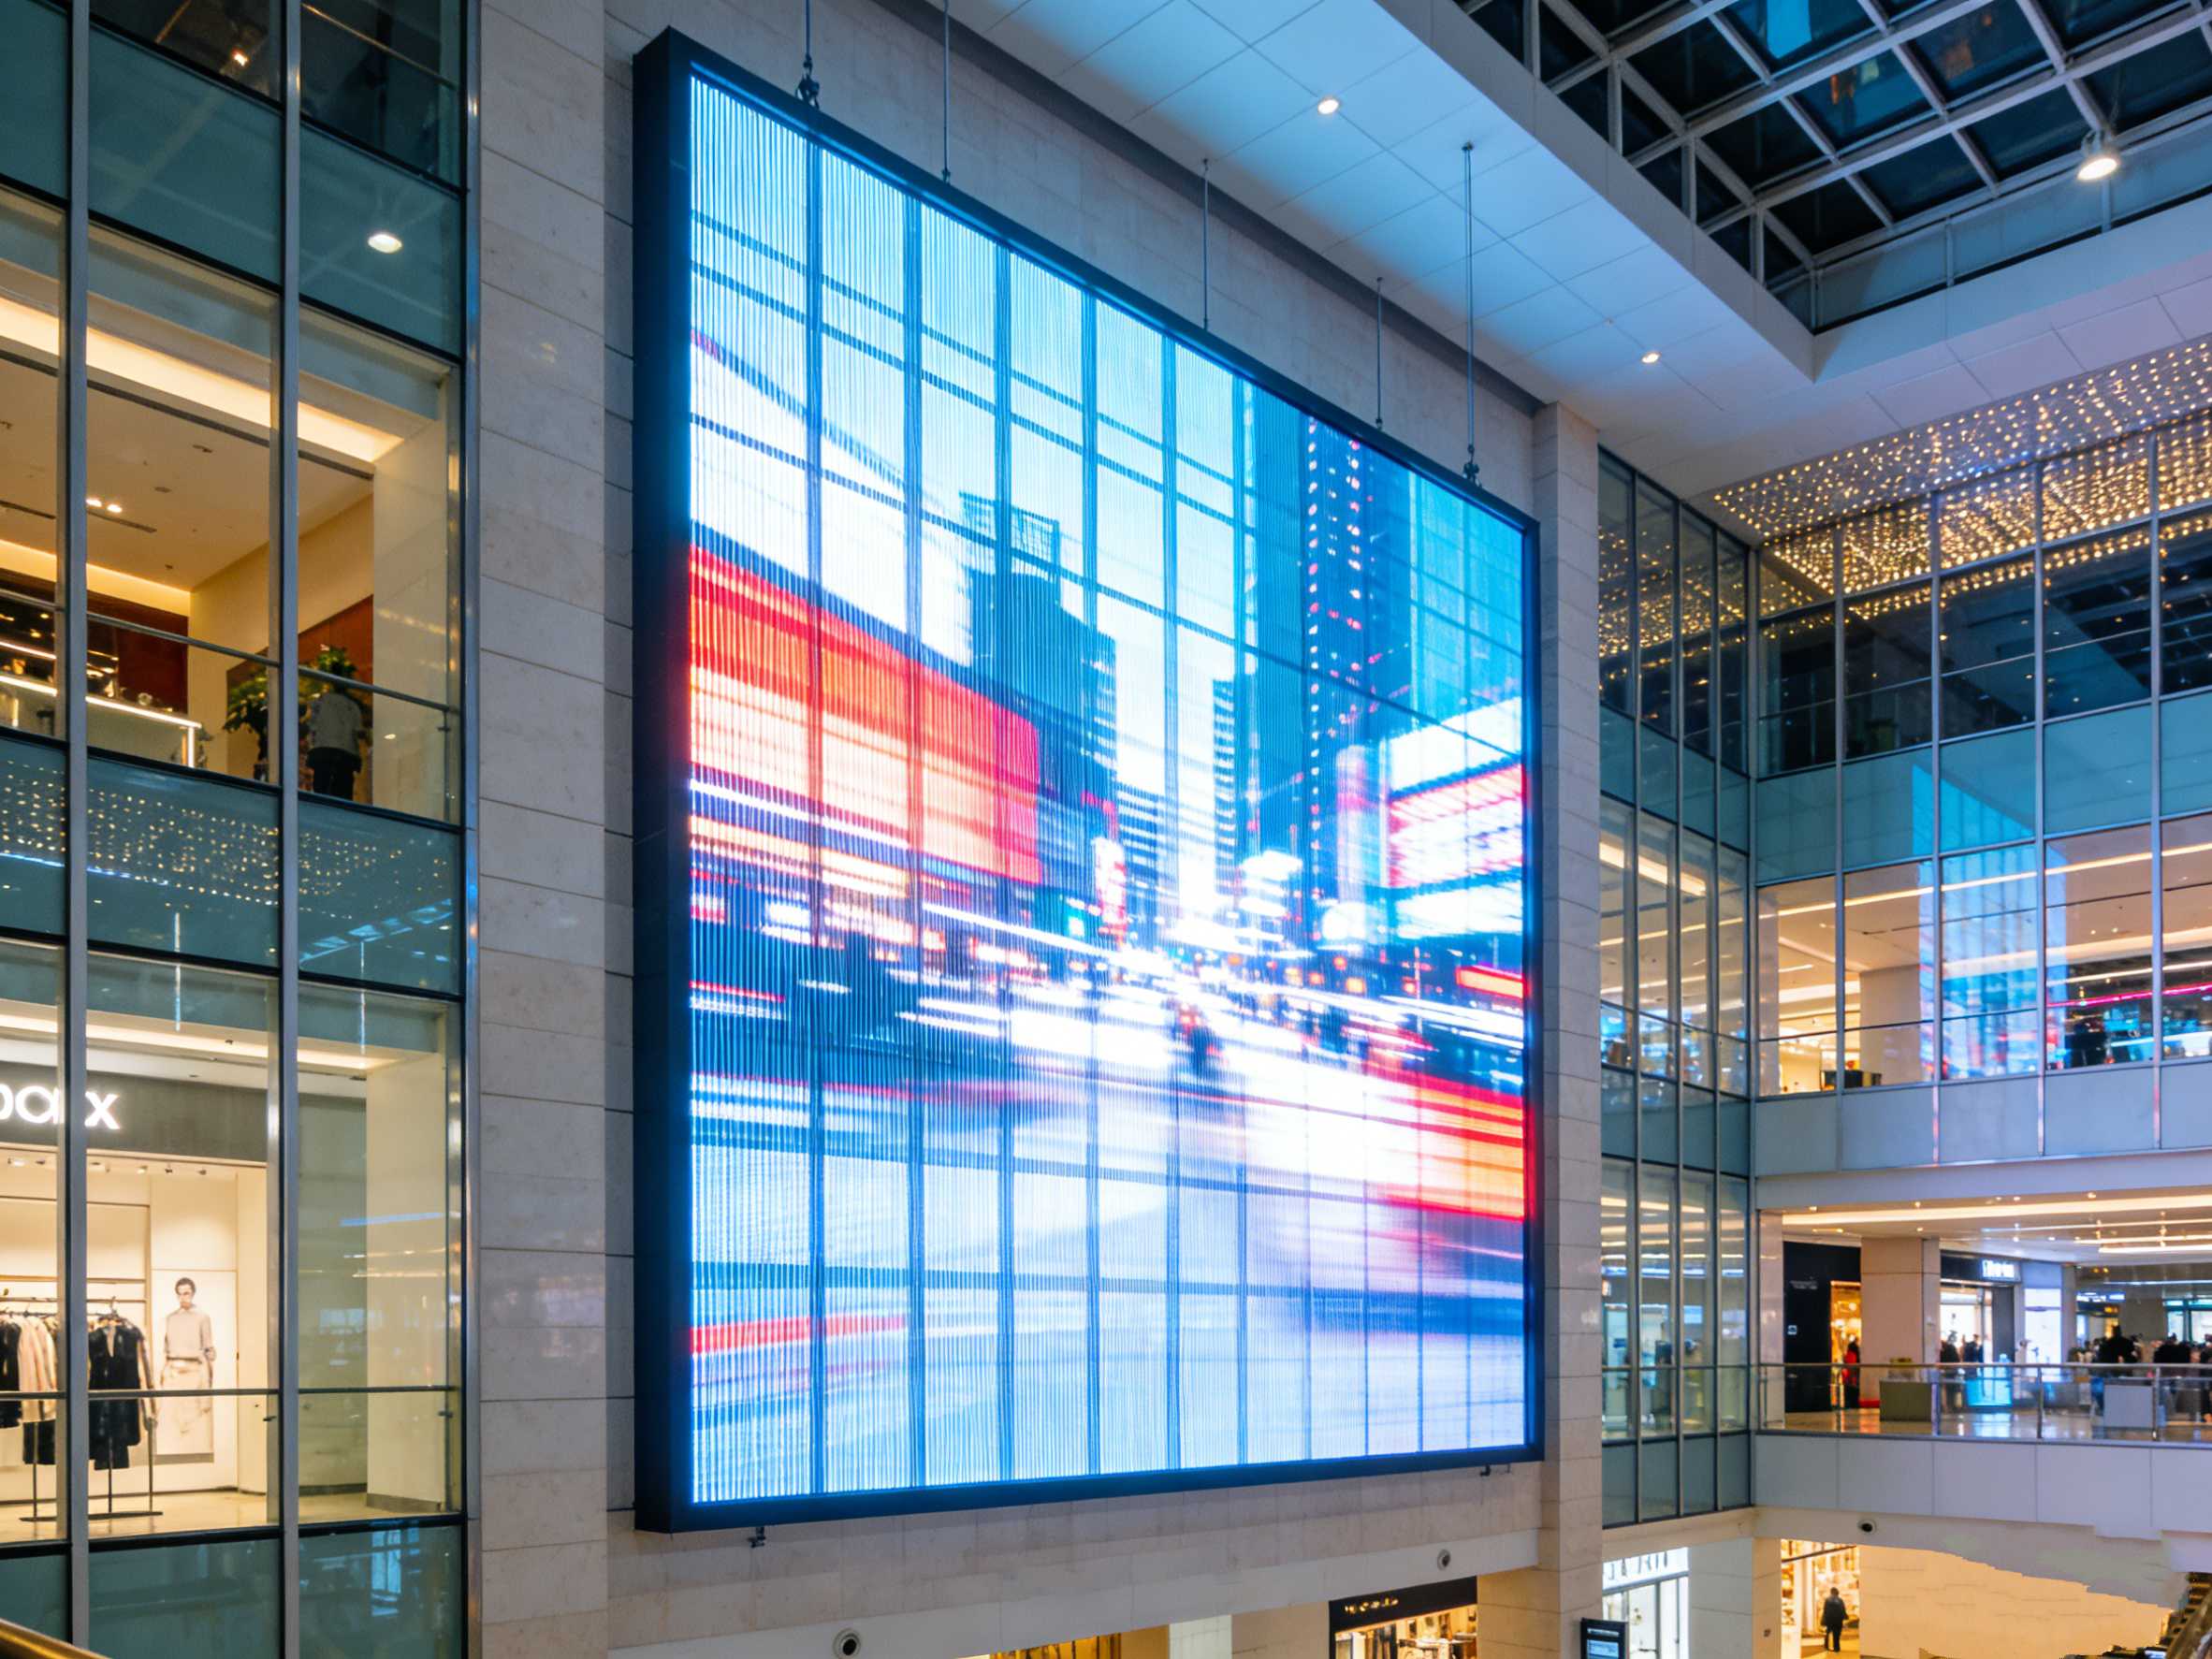
A major source of confusion in procurement comes from vendors grouping three completely distinct technologies under the broad marketing term "glass LED display." When we are using these systems in real architectural environments, picking the wrong technology category will instantly violate structural facade building codes or fail landlord tenant-fitout regulations.
Here is the plain breakdown of how these three hardware formats actually differ in their physical construction:
Architectural Laminated Photoelectric LED Glass (True LED Glass):
This format sandwiches surface-mount micro-LEDs and invisible laser-etched conductive traces directly between two layers of architectural tempered glass. The assembly is permanently bonded inside an industrial autoclave under high temperature and vacuum pressure using PVB (Polyvinyl Butyral) or SGP (SentryGlas) interlayers. The finished product is not an accessory hung onto a window; it is the physical window itself, capable of serving as a primary facade curtain wall, structural glass railing, skylight canopy, or interior partition wall. It delivers maximum weatherproofing, physical security, and architectural clean lines, but carries zero field repairability for individual diodes—meaning module manufacturing redundancy is critical.
Adhesive Transparent LED Film (Stick-On Flexible Glass Displays):
This technology deposits micro-diodes onto an ultra-thin, flexible PET or polyimide optical film coated with a pressure-sensitive optical clear adhesive (OCA). It is designed to be pasted directly onto the interior surface of existing architectural glass windows, much like window tint film. It is lightweight, flexible, and causes minimal impact to building structures. However, it cannot serve as architectural glass on its own, it is vulnerable to edge peeling and mechanical scratching, and the optical adhesive can turn yellowish if exposed to intense, unmitigated solar UV radiation over several years.
Suspended Transparent LED Bar/Strip Glass Screens:
This format uses rigid, ultra-thin aluminum or PCB louvers mounted onto a lightweight aluminum frame that hangs 50mm to 100mm directly behind an existing glass curtain wall. While technically not made of glass, many buyers call it a "glass display" because it mounts directly against window glazing. It delivers massive brightness (often 6,000 to 8,000 nits) and easy modular maintenance, but it adds structural dead load behind the glass, produces noticeable rear glare inside tenant spaces, and leaves horizontal visual stripes when seen up close.
Some friends want to know which product architecture actually suits their structural load limits, lighting environment, and long-term maintenance reality. Detailed setup methods and engineering comparisons make all the difference, so let's look at the technical parameters side-by-side:
| Engineering Parameter | Structural Laminated LED Glass | Adhesive Optical LED Film | Suspended Glass-Backing Bar Screen |
|---|---|---|---|
| Physical Construction | Dual-pane tempered glass + SGP/PVB | Flexible PET film + optical adhesive | Aluminum louver frames behind glass |
| Typical Pixel Pitch (P) | P6.0 mm – P20 mm | P3.91 mm – P16 mm | P2.8 mm – P10 mm |
| Visual Transmittance Rate | 80% – 92% (Maximum transparency) | 75% – 88% | 65% – 82% |
| Peak Calibrated Brightness | 3,500 – 6,000 nits | 2,000 – 4,000 nits | 5,000 – 7,500 nits |
| Structural Certification Level | Certified Architectural Safety Glass | Interior decorative surface finish | Non-structural suspended AV fixture |
| Weight per Square Meter | 28 – 45 kg (Replaces heavy glass) | 1.8 – 3.5 kg (Extremely lightweight) | 10 – 16 kg (Added dead load on mullions) |
| Ultraviolet (UV) Resistance | Exceptional (UV-filtering interlayers) | Moderate (Adhesive oxidizes over time) | High (Powder-coated aluminum + anti-UV PC) |
| Water & Moisture Ingress Rating | True IP67 / IP68 (Hermetically sealed) | IP43 – IP54 (Interior rated only) | IP30 rear / IP65 front (Application dependent) |
| Operating Temperature Range | -30°C to +85°C | -10°C to +55°C | -20°C to +60°C |
| Field Maintenance Strategy | Panel replacement or trace redundancy | Strip peel-and-replace | Quick-release individual louver swap |
| Manufacturing CapEx Profile | Premium investment (Cleanroom / Autoclave) | Mid-to-high initial cost | Economical to mid-range baseline |
| Best Architectural Application | Building facades, canopies, glass balustrades | Retail window fitouts, office partitions | Giant outdoor DOOH glass wall retrofits |
When evaluating overseas glass led display manufacturers, low quotes are always tempting on paper. What I always use in the field to identify high-risk suppliers is an audit of four internal failure points that brokers and small workshops hide behind polished rendering videos:
The EVA vs. PVB/SGP Interlayer Substitution: In architectural glass manufacturing, laminating interlayers determine structural longevity. Top-tier architectural glass makers use thermosetting PVB or structural ionoplast interlayers like Kuraray SentryGlas (SGP). SGP provides five times the tear strength and one hundred times the rigidity of standard laminates, preventing moisture creep and edge delamination even in humid subtropical climates. Cut-rate suppliers substitute cheap solar-grade EVA (Ethylene Vinyl Acetate). EVA softens at lower temperatures, outgasses volatile organic compounds that degrade the LED packaging epoxy, and develops milky micro-bubbles and edge delamination after eighteen months of exposure to high solar radiation.
High-Resistance Transparent Conductive Traces: To achieve visual transparency, the electrical circuits feeding power and data to the LEDs must be nearly invisible. Quality manufacturers use photolithography-patterned ultra-fine metal mesh (copper or silver mesh traces narrower than 10 microns) or high-conductivity magnetron sputtered Indium Tin Oxide (ITO). Bargain factories use low-grade screen-printed conductive pastes with high internal sheet resistance (Rs > 30 Ω/sq). When you power up the display, high electrical resistance produces a massive voltage drop across the glass lite, causing noticeable brightness loss from the bottom of the panel to the top, accompanied by internal hot spots that cook the diodes inside the lamination.
Use of Standard Indoor Mini-LED Packages: Outdoor-facing glass facades are exposed to intense ambient sunlight, high thermal spikes, and UV radiation. Reliable builders select specialized outdoor-rated micro-LED packages with gold-wire bonding, black matrix encapsulation for high contrast, and UV-inhibited epoxy cups. Less ethical suppliers solder standard commercial indoor SMD diodes onto the transparent substrate. Under daily solar UV exposure, standard packaging resin oxidizes rapidly, shifting the color temperature from a clean 6500K white to a muddy yellow within twelve months.
Undersized Power Injection and Overheated Driver Routing: Because glass is an electrical insulator and a poor thermal conductor, driver ICs cannot be buried inside the laminated glass sandwich. Quality systems place driver ICs and power step-down converters inside the concealed aluminum architectural perimeter profiles, using active thermal management. Cheap builders attempt to glue driver chips directly onto glass edges without adequate thermal heat-sinking. In summer, the aluminum mullion channels reach 65°C, triggering thermal throttling in the driver ICs, leading to flickering panels and catastrophic column failure across the screen.
Detailed verification steps make all the difference, so let's look at the testing protocol. When you receive custom glass LED evaluation samples or fly to a production plant for factory acceptance testing (FAT), never rely on short promotional video loops. Follow this systematic testing sequence to expose latent manufacturing defects:
Thermal Shock and Autoclave Bubble Stress Test
Place a laminated glass test lite (at least 600mm × 600mm) inside an environmental test chamber. Cycle the temperature rapidly between -30°C and +85°C with a two-hour dwell time at each extreme, repeating the cycle for forty-eight continuous hours while maintaining 85% relative humidity. Inspect the perimeter edges and the areas immediately surrounding the LED diodes under 20x optical magnification. Look for microscopic air bubbles, resin hazing, or adhesive separation between the glass, interlayer, and circuit substrate.
Low-Grayscale Uniformity and Voltage Drop Mapping
Connect the glass display panel to a precision power analyzer and a master video processor. Lower the brightness down to 5%, 10%, and 15% across pure gray, red, green, and blue test screens. Low-grayscale test screens immediately reveal variations in trace resistance, driver IC response time, and diode forward voltage (Vf) mismatches. The panel must show uniform illumination across the entire glass surface with zero vertical streaks, flickering rows, or brightness drop-offs between the power edge and the floating center.
High-Voltage Dielectric Breakdown Test (Hi-Pot Test)
Architectural glass displays must meet strict building electrical safety standards. Connect a calibrated dielectric breakdown tester between the active transparent circuit bus and the structural aluminum framing or outer glass edge. Apply 1,500V AC for sixty seconds. The measured leakage current must remain below 5mA with zero dielectric breakdown or electrical arcing. Passing this test proves that the internal electrical insulation will not short out to the building frame during heavy rain or lightning storms.
Off-Axis Optical Haze and Color Distortion Sweep
Position an optical spectrometer on a motorized goniometer arm or mount a calibrated digital lux meter on a tripod. Measure the display output from perpendicular (0°) out to an acute 70° angle along both horizontal and vertical axes while playing a full-white (6500K) video pattern. High-quality transparent glass panels retain at least 65% of their on-axis brightness at 60° off-axis with less than a 250K color temperature shift. Inferior conductive films or cloudy interlayers produce massive optical haze, chromatic aberrations, and halo rings around the diodes.
Structural Lamination and Ball Impact Verification
Demand third-party laboratory test reports certifying compliance with ANSI Z97.1 (American National Standard for Safety Glazing Materials) or European EN 12600 pendulum impact standards. For overhead skylight or structural balustrade deployments, request drop-ball impact test verification (dropping a 2.27 kg smooth steel ball from a height of three meters onto the center of the laminated test glass). The glass may fracture under extreme impact, but the interlayer must retain all glass fragments with zero through-penetration, proving structural life-safety compliance.
To make informed decisions, let's explore three critical questions that every facade engineer, structural consultant, and project director must resolve:
This is the most critical question in the industry. Because true photoelectric LED glass is laminated into a single solid unit inside an autoclave, you cannot desolder and replace an individual diode on-site without destroying the glass panel. High-tier glass led display manufacturers resolve this through two engineering strategies:
Circuit Redundancy and Dual-Wire Signal Paths: Premium designs feature redundant parallel micro-circuits for both data and power. If a single LED die experiences an open-circuit failure, an automatic bypass diode within the packaging allows data and electrical current to jump past the defective diode, preventing the loss of the rest of the column.
Modular Panel Partitioning: The overall display facade is divided into independent, standardized architectural glass units (IGUs) matching the building's structural mullion spacing. If a glass unit suffers physical glass breakage or multiple diode failures over years of operation, the entire laminated panel is swapped out from the building interior using standard glazing suction cups, just like replacing a cracked architectural window pane.
In commercial architectural facades, building energy codes (such as ASHRAE 90.1 or European Energy Performance of Buildings Directive) require high thermal insulation, specified by strict U-values and Solar Heat Gain Coefficients (SHGC). You cannot compromise these energy metrics to install a display.
Professional manufacturers integrate photoelectric glass as the inner lite of a double-glazed or triple-glazed Insulated Glass Unit (IGU). The outer lite carries a high-performance Low-E (low-emissivity) solar control coating, separated from the inner LED glass lite by a 12mm to 16mm sealed cavity filled with inert Argon gas and molecular sieve desiccant. Crucially, the Low-E coating must be positioned on Surface #2 (inside of the outer glass pane) to reflect exterior solar heat while ensuring that the LED light emitted from the inner pane passes unobstructed outward to the street.
Yes, and this happens more often than many people realize. In North America and Europe, exterior building envelopes are tightly regulated. Fire and building safety codes require all materials on exterior walls to comply with ASTM E84 / UL 723 (flame spread and smoke development) and NFPA 285 (fire propagation characteristics of exterior wall assemblies). If you import uncertified glass panels containing non-compliant resin interlayers, or panels that lack an accredited NRTL electrical safety certification (such as UL 8750 or UL 62368-1), the local building inspector can issue an immediate Stop Work Order or deny the building's final Certificate of Occupancy (CO). Always demand to see the factory's active UL file number, and independently verify that the certificate matches the exact physical construction of the glass assembly being supplied.
When evaluating quotes from overseas manufacturers, remember that the bare glass panels represent only part of the capital deployment. Here is a realistic budget allocation breakdown for a complete commercial architectural glass LED facade:
Custom Laminated LED Glass Panels & Interlayers (48% – 55% of Total Cost): This encompasses high-spec ultra-clear low-iron float glass (such as PPG Starphire or CSG low-iron), automated photolithography metal-mesh or ITO circuit printing, high-binning outdoor micro-LED packages, SGP structural interlayers, and high-pressure autoclave laminating cycles.
Concealed Profile Frames, Brackets, & Structural Glazing (12% – 16% of Total Cost): Custom-extruded, anodized or PVDF-coated aluminum mullion profiles designed to house perimeter driver boards, wiring conduits, structural silicone glazing seals (such as Dow Corning 995), and stainless steel anchor brackets.
Video Processing, Sending Infrastructure, & System Redundancy (10% – 14% of Total Cost): Flagship master video controllers (NovaStar COEX series, Brompton, or Colorlight), fiber-optic distribution nodes, low-latency scaling processors, and optical video distribution matrixes configured for 100% redundant loop architecture.
High-Efficiency Power Distribution & Smart PDU Units (8% – 11% of Total Cost): Centralized, high-efficiency common-cathode DC power supply banks (often installed in an accessible remote IT room up to 15 meters away to eliminate heat behind the glass), intelligent power distribution cabinets with sequential relay switching, and surge suppression.
Spare Unit Provisioning Package (6% – 8% of Total Cost): A project-specific safety inventory containing 3% to 5% fully assembled, pre-calibrated spare glass panels from the exact same manufacturing production run and silicon wafer lot, plus 10% spare driver boards and power modules.
Heavy-Duty Sea Freight Crating & International Logistics (4% – 6% of Total Cost): Custom-built, ISPM-15 certified non-fumigation plywood A-frame glass crates lined with high-density neoprene shock buffers, desiccant packs, and continuous shock and tilt recording sensors to prevent handling damage during ocean transit.
When managing architectural display installations, the most dangerous mistake a project lead can make is treating active photoelectric glass like standard commercial LED cabinets where you simply pick the cheapest supplier on an internet directory. Architectural glass is a permanent building component. Once structural silicone cures and the building curtain wall is pressurized, replacing an improperly manufactured, delaminating glass panel costs ten to twenty times the original unit price of the panel itself in scaffolding, mobile crane rental, and traffic disruption permits.
My practical recommendation is clear: always insist that the manufacturer write your performance specifications directly into the binding master supply contract. Mandate the use of authentic Kuraray SGP structural interlayers or premium automotive-grade PVB, specify branded gold-wire micro-LED diodes with single-batch wavelength grouping (±1.5nm tolerance), and require common-cathode driver architecture to keep thermal generation to an absolute minimum.
Make milestone payments conditional on performance: release the final 20% balance only after the complete screen has passed an on-site 72-hour full-load burn-in test without dead pixels or thermal hot spots. Finally, ensure the manufacturer delivers an archived digital copy of the factory optical calibration coefficient files (.rcfgx or vendor equivalent) tagged to each specific panel serial number. This way you can replace a damaged glass unit five years down the road, push the stored calibration data over your network, and keep your building facade visually seamless and uniform without distracting patch marks. Hope this helps you navigate vendor negotiations with complete technical clarity.
Because laminated photoelectric glass requires custom laser patterning, bespoke photolithography masks, and autoclave tooling setups, established manufacturers generally set an MOQ between 30 and 50 square meters for custom architectural glass dimensions. For standard off-the-shelf catalog panels or pre-engineered modular partition sizes, some factories will accept prototype evaluation orders starting around 10 square meters.
Standard clear float glass contains natural iron oxide impurities that create a distinct greenish tint along the edges, absorbing roughly 8% to 12% of visible light and altering the color balance of outgoing video. Low-iron glass (often called extra-clear or opti-white glass) reduces iron content to less than 0.01%, providing over 91% light transmittance, zero green tint, and true color reproduction for commercial brand graphics.
Power is transmitted across the glass lite using transparent conductive coatings (like magnetron-sputtered Indium Tin Oxide) or microscopic etched metal-mesh grids that are virtually invisible to the human eye from normal viewing distances. At the panel perimeter, these transparent traces transition into thin, concealed copper busbars embedded inside the black ceramic frit border of the glass, connecting to driver boards hidden inside the aluminum mullion channels.
No. Like all fully tempered architectural safety glass, laminated photoelectric LED glass cannot be cut, notched, or drilled after undergoing the thermal tempering and lamination process. Any attempt to cut or drill the glass on-site will release internal surface compressive stresses and instantly shatter the entire tempered glass panel. All structural holes, notches for door handles, and cable egress ports must be precision CNC-machined prior to tempering.
For North America, the glass must comply with ANSI Z97.1 and CPSC 16 CFR 1201 for architectural safety glazing, alongside UL 8750 / UL 62368-1 for electrical equipment safety and FCC Part 15 Class B for electromagnetic interference. For the European Union, the product must carry valid CE markings backed by declarations of conformity for EN 12150 (tempered glass), EN 14449 (laminated glass), the Low Voltage Directive (LVD 2014/35/EU), and the EMC Directive (2014/30/EU).
High-grade photoelectric glass displays engineered with gold-wire LED dies, SGP structural interlayers, and remote common-cathode power supplies have an operational design lifespan rated at 100,000 hours to half-brightness (L50 standard). Under normal commercial operation of 14 to 16 hours per day at calibrated brightness, this translates to approximately 10 to 12 years of reliable performance before diode degradation becomes noticeable.
On tall commercial high-rises, exterior curtain walls endure immense positive wind pressure and negative suction loads (often exceeding 2.5 to 4.0 kPa during typhoons or hurricane-force storms). Glass LED manufacturers must calculate total glass thickness (such as 8mm + 1.52mm SGP + 8mm configurations) and panel deflection limits according to local building codes (like ASTM E1300) to ensure the glass does not flex excessively, which could snap the internal micro-electronic traces.
Yes, this is the standard installation method for exterior building envelopes. The laminated photoelectric LED panel serves as the interior structural lite, paired with an exterior pane of tempered solar-control glass. The two lites are bonded around an insulated warm-edge spacer bar with primary polyisobutylene (PIB) and secondary structural silicone seals, creating a hermetically sealed gas space filled with Argon to meet strict building energy U-value requirements.
Because the manufacturing sequence involves precision CNC glass cutting, edge polishing, ultrasonic cleaning, photolithography circuit printing, SMT micro-placement, cleanroom pre-lamination, and high-pressure autoclave baking, standard production lead time typically spans 35 to 50 business days following shop drawing approval. Ocean freight to West Coast US ports requires approximately 18 to 22 days, while transit to European main ports takes roughly 28 to 35 days.
Panels must be shipped in custom heavy-duty, non-fumigation plywood A-frame crates constructed to ISPM-15 standards. Individual glass lites must be separated by protective cork pads or high-density polyethylene interleaving foam sheets to prevent friction scratching. The exterior of each crate should feature waterproof heavy-duty plastic wrapping, desiccant packs inside the framing, and external tamper-evident shock and tilt monitoring indicators to immediately document any rough handling during ocean transit.