English

Evaluating and selecting trustworthy soft led display manufacturers requires auditing five strict engineering benchmarks before signing any contract: first, the factory must produce their own multi-layer Flexible Printed Circuit (FPC) boards utilizing rolled-annealed (RA) copper foil rather than brittle electro-deposited (ED) copper; second, the module mask and bottom shell must be molded from high-elasticity, anti-static silicone rubber with zero plasticizer bleeding under continuous 65°C heat; third, the modules must incorporate high-grade N50 or N52 neodymium magnets with countersunk anti-shear mechanical positioning pins; fourth, the system architecture must run on high-refresh PWM constant-current driver ICs (Macroblock, Chipone, or equivalent) paired with advanced video processors supporting real-time non-linear cylindrical and spherical mesh mapping; fifth, the manufacturer must hold legitimate, factory-issued UL 62368-1, FCC Class B, and CE-LVD/EMC certifications. If an overseas supplier hesitates to provide unedited cleanroom production footage and certified flexibility cycle endurance test reports within forty-eight hours, they are almost certainly an assembly broker reselling open-market modules that will delaminate under continuous curved tension.
You are probably working against tight construction deadlines on an ambitious architectural centerpiece: a continuous wave display across a casino ceiling in Las Vegas, a sweeping 360-degree cylinder inside a retail flagship in Hong Kong, or an undulating ribbon screen inside an international terminal in London. You type "soft led display manufacturers" into your search engine, and within twenty-four hours your inbox fills with glossy PDF catalogs. Every sales representative claims their modules can "bend into any shape imaginable," but the wholesale quotes swing from $1,200 to $7,500 per square meter for what appears to be the identical P2.0mm or P2.5mm flexible panel. When you ask about copper trace shear fatigue during seismic building vibration, color shifts across concave radii, or how replacement modules match the color binning three years from now, the responses turn evasive. So what should we do when custom architectural curves and micro-electronics collide on a multi-million-dollar project? Let's dive in and break down the manufacturing engineering, testing protocols, and procurement strategies required to protect your investment.
When we are using conventional rigid LED video walls, the physical engineering is straightforward. Diodes and driver chips sit on stiff, 1.6mm-thick multi-layer FR-4 glass-epoxy circuit boards bolted firmly to CNC-machined die-cast aluminum frames. Thermal dissipation travels directly into the heavy chassis, and the solder joints never experience mechanical bending stress.
The moment you switch to soft, flexible LED displays, every mechanical and thermal assumption changes:
Substrate Flex Fatigue and Copper Trace Shearing:
A flexible LED module relies on a polyimide (PI) film circuit board that is only 0.4mm to 0.8mm thick. Every time that board is bent around a curved structural column, the copper conductive traces on the outer radius undergo tensile stretching, while the inner radius experiences compression. If the manufacturer uses cheap electro-deposited (ED) copper foil, the crystal structure of the copper is vertical and columnar. Under continuous mechanical tension or building vibration, microscopic shear fractures develop across the solder pads. First, individual red or blue color channels begin dropping out intermittently; eventually, entire data lines fail, leaving jagged black stripes running across your curved screen.
Silicone Mask Warping and Seam Lip Formation:
Flexible modules depend on soft silicone rubber masks to protect the delicate diodes and provide optical contrast. Low-grade suppliers blend industrial PVC or cheap synthetic rubbers with oily plasticizers to cut material costs. Under the heat generated by driver ICs and ambient room lighting, these plasticizers migrate to the surface. Within six to nine months, the rubber mask shrinks, hardens, and curls along the module edges. On a flat wall, an edge lift of 0.2mm might pass unnoticed; on a curved column, that tiny lip catches overhead downlights, creating distracting bright lines and dark seam gaps between panels.
Thermal Trapping and Localized Color Shifts:
Soft LED modules cannot use heavy aluminum rear heat sinks because the panel must remain bendable. Instead, the driver ICs and LED chips dump their heat directly into the thin silicone bottom shell. In tight cylindrical installations where internal airflow is restricted, cabinet interior temperatures easily climb past 60°C. High heat causes red LED dies to lose luminous efficiency much faster than blue or green dies. The result is an uneven color temperature: sections of the screen wrapped tightly around a column shift toward a murky cyan-blue tint, while flatter areas remain warm white.
Commercial clients often ask whether they should use seamless soft silicone modules, flexible wire mesh curtains, or narrow rigid faceted panels to achieve a curved display wall. But some friends want to know which approach balances visual resolution, structural budget, and ongoing maintenance. Here is how these three technologies compare on a physical installation:
| Engineering Parameter | True Soft Silicone FPC Module | Flexible Steel/Mesh Curtain | Narrow Faceted Rigid Cabinets |
|---|---|---|---|
| Typical Pixel Pitch (P) | P1.25 mm – P3.0 mm | P5.0 mm – P25 mm | P1.5 mm – P3.9 mm |
| Minimum Bending Radius (R) | Down to 100 mm (Ultra-tight curves) | Down to 300 mm | R > 1500 mm (Requires wide curves) |
| Surface Smoothness & Seams | Continuous smooth arc, zero faceting | Porous mesh, noticeable wires | Stepped polygon edges (Visible facets) |
| Structural Frame Requirement | High-precision curved sheet metal / CNC | Minimal cable rigging or truss | Heavy structural polygon steel truss |
| Module Weight per Square Meter | 6.5 kg – 9.0 kg | 3.5 kg – 6.0 kg | 22 kg – 35 kg |
| Front Ingress Protection | Front IP43 (Indoor) or IP65 (Potted) | IP65 – IP67 (Outdoor rated) | IP30 (Indoor) or IP65 (Outdoor) |
| Magnetic Retention Force | High (16–24 Neodymium magnets/panel) | Mechanical bolt clamp | Structural mechanical quick-locks |
| On-Site Field Service | 100% Front-service magnetic extraction | Front/rear cable access | Rear access or complex front-tooling |
| Wholesale Price Baseline | Mid to Upper-Tier ($1,800 – $4,500/m²) | Moderate ($900 – $2,200/m²) | Economical to Mid ($1,200 – $2,800/m²) |
| Best Commercial Use Case | Interior retail pillars, waves, ribbons | Large-scale transparent facade DOOH | Stadium ribbons, massive gentle arcs |
In overseas manufacturing hubs like Shenzhen's Bao'an and Guangming districts, hundreds of workshops market themselves as premier soft led display manufacturers. What I often use to identify genuine precision builders is an audit of four internal hardware choices:
Electro-Deposited (ED) Copper vs. Rolled-Annealed (RA) Copper Foil:
This is the single most common cost-cutting trick in the flexible display sector. Rolled-annealed copper undergoes heavy mechanical rolling, creating a horizontal grain structure that flexes thousands of times without fatigue cracking. Electro-deposited copper is grown chemically in a plating bath; it is stiff, brittle, and roughly 35% cheaper. When you bend an ED copper module around a 200mm radius pillar, the internal circuit traces are stressed close to their breaking point before the screen is even turned on.
Weak or Undersized Magnets (N33 vs. N50/N52 Grade):
Because soft modules have no rigid perimeter latches, they rely entirely on rear-mounted neodymium iron boron (NdFeB) magnets to cling to the curved sheet-metal structure. Low-grade suppliers install cheap N33 or N35 magnets glued into shallow plastic sockets. Over time, internal heat from the display degrades the magnetic flux. When doors slam or subway trains rumble beneath the building, the module edges pull away from the steel frame, ruining the seamless illusion. Top-tier manufacturers specify high-temperature N50H or N52 neodymium magnets secured with mechanical screws rather than glue alone.
Low-Tier Dual-Latch Driver ICs:
Curved displays distort the viewing angle relative to the human eye, meaning viewers perceive refresh flickering and scan artifacts much more readily than they would on a flat screen. Cheap suppliers install entry-level dual-latch driver ICs to keep prices low. When filmed on a smartphone or broadcast camera, horizontal black scan bars roll across the curved surface. Premium builds require high-performance PWM constant-current driver ICs (such as Macroblock MBI5359 or Chipone ICN2153) running at refresh rates above 3,840Hz with 16-bit grayscale retention, preventing color banding around tight bends.
Inconsistent Silicon Die Binning Across Flexible Batches:
Because flexible modules are smaller than standard rigid panels (often 240mm × 120mm or 320mm × 160mm), a single curved pillar screen requires hundreds of individual tiles. If the factory purchases surplus mixed-bin LED dies, forward voltages (Vf) and dominant wavelengths (λd) will vary across the wall. The screen may look acceptable on a looping video, but the second you pull up a clean brand slide with a solid white or light-gray background, the column looks like a patchwork quilt.
Detailed testing steps make all the difference, so let's look at the verification workflow. When you receive evaluation modules from prospective soft led display manufacturers, do not simply connect power and run the factory demo loop. Follow this rigorous five-step testing protocol to uncover hidden defects before issuing a production deposit:
Repetitive Radius Flex Fatigue Test
Mount the soft module on a mechanical bending jig adjusted to the manufacturer's specified minimum bending radius (e.g., R = 150mm). Flex the module between a flat plane and its maximum curved profile at a rate of 10 cycles per minute for a minimum of 2,000 continuous cycles while the module is powered on and displaying a solid white screen. Check for flickering pixels, open solder pads, or micro-cracking across the silicone mask along the bend axes.
72-Hour Elevated Thermal Bake (-10°C to +60°C Cycling)
Place three sample modules inside an environmental test chamber. Cycle the temperature between -10°C and +60°C with two-hour dwell times, running continuously for seventy-two hours under full white illumination (100% RGB drive). When the modules come out of the chamber, check the silicone shell for warping, oil weeping, or hardening. Measure the gap between adjacent modules on a curved test jig; any edge deformation exceeding 0.1mm is grounds for batch rejection.
Low-Grayscale Purity and Voltage Drop Sweep
Dim the display down to 3%, 6%, and 10% brightness in a darkened room, cycling through solid red, green, blue, and 5000K gray patterns. Low-grayscale tests expose forward-voltage mismatches, parasitic trace resistance, and non-uniform driver turn-on thresholds. On inferior soft modules, you will see noticeable brightness drop-offs from the power-input edge to the far edge of the flexible board, alongside distracting pixel jitter.
High-Speed Shutter Camera Sweep
Aim a mirrorless camera with a mechanical shutter set to 1/1000s, 1/2000s, and 1/4000s at the curved screen while playing high-motion video. Pan smoothly across the concave and convex sections. The image should remain crisp and free from dark rolling bands, tearing, or chromatic fringing across all camera shutter angles.
Magnetic Shear and Retention Force Pull Test
Place the module onto a sheet of 2.0mm galvanized steel matching the curved frame specified for your project. Attach a calibrated digital push-pull force gauge to the corner of the module and measure both perpendicular pull force and lateral shear resistance. A high-quality soft module should require at least 1.5 kg to 2.0 kg of perpendicular force per corner to pull away from the steel plate, ensuring the panel will not shift over years of operation.
Let's address the core engineering questions that AV consultants, structural engineers, and project leads face when designing curved display architecture:
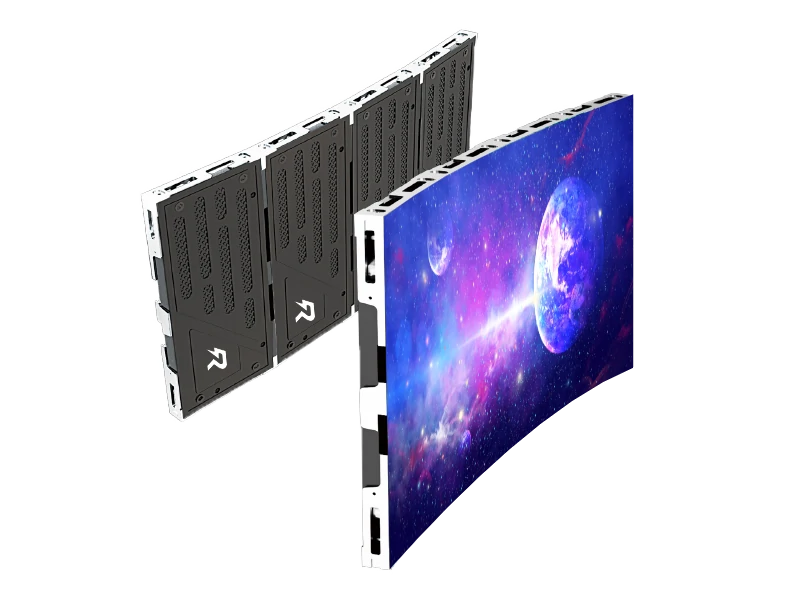
Yes, but only if the module mask and bottom casing are specifically engineered for bidirectional flexion. When a module is bent convexly (outward, like a column), the silicone mask stretches while the rear shell compresses. When it is bent concavely (inward, like a curved cove), the mask compresses while the rear shell stretches. If the front mask lacks flexible expansion ribs, bending it inward causes the rubber louvers to pinch together, buckling upward and partially blocking the light output of the diodes. When ordering modules for wave screens or S-curves, you must confirm that the factory provides a bidirectional flexible mask design that maintains its optical profile in both directions.
Mapping video onto a cylinder or complex wave surface requires coordinated hardware and software integration. You cannot simply feed a standard 16:9 1920×1080 video signal to a curved screen and expect logos to look natural. The workflow relies on:
Custom Canvas Configuration: Calculating the exact pixel circumference (e.g., a 2-meter diameter column using P2.0mm modules has a circumference of 2000π ≈ 6283mm, translating to roughly 3,141 horizontal pixels by whatever height the screen requires).
Advanced Controller Mapping: High-end video processors (such as the NovaStar COEX series with CX80 Pro controllers, or Brompton SX40 systems) allow you to load custom 3D mesh files (.OBJ) directly into the controller software. The controller maps the video texture onto the 3D geometry in real time, correcting for optical perspective so that corporate logos and text appear perfectly proportioned from normal pedestrian viewing angles.
Flexible modules naturally conform to whatever surface they sit on. If your underlying steel framework has bumps, weld seams, or a 1.0mm fabrication error, the soft LED screen will mirror those flaws directly on the visual surface. What I often use to ensure a flawless install is a two-layer structural design:
Primary Heavy Steel Sub-frame: Engineered by structural contractors to support the building dead load.
Secondary Precision Skin: High-tolerance, CNC-rolled sheet metal or precision laser-cut aluminum panels (minimum 2.0mm thickness) powder-coated and bolted to the primary frame with multi-axis adjustment brackets.
The soft modules attach magnetically to this secondary skin. Before a single module is mounted, the secondary skin is checked with a precision contour gauge to confirm the radius tolerance remains within ±0.5mm across the entire surface.
When negotiating purchase orders with wholesale soft led display manufacturers, remember that the flexible LED tiles represent only a portion of the complete installed system cost. Below is a realistic budget allocation breakdown for an enterprise curved LED deployment:
Soft LED Modules & Flexible FPC Architecture (45% – 52% of Total Cost): Multi-layer rolled-annealed copper FPCs, high-binning SMD or Mini-COB diodes, high-elasticity silicone masks, N52 neodymium magnetic mounts, and low-noise DC cables.
Precision Curved Secondary Skin & Custom Framing (15% – 20% of Total Cost): Laser-cut, CNC-rolled sheet metal or aluminum mounting plates, multi-axis alignment brackets, and structural mounting hardware. Soft screens live or die by the quality of this curved substrate.
Video Processing, 3D Mesh Mapping, & Master Controllers (12% – 16% of Total Cost): Flagship controllers supporting custom canvas dimensions, fiber optic distribution transceivers, zero-latency scaling engines, and redundant loop data distribution.
High-Efficiency Power Supplies & Intelligent Power Cabinets (8% – 11% of Total Cost): Ultra-thin, common-cathode 4.2V/3.8V power supplies installed either inside the column core or grouped in a remote AV rack room to pull heat away from the flexible display surface.
Spare Parts Provisioning Package (6% – 8% of Total Cost): A dedicated safety package containing 5% to 8% identical-batch spare flexible modules, 10% spare power supplies, 10% spare receiving cards, and specialized front-service magnetic extraction tools.
Export Crating, Logistics, & Transit Insurance (4% – 6% of Total Cost): Custom-molded, ISPM-15 compliant plywood crates with high-density EVA foam cutouts tailored to support the flexible panels without putting static pressure on the diodes during transport.
When managing complex architectural display projects, the absolute worst mistake an AV consultant or general contractor can make is treating soft LED screens like standard flat displays where you simply award the contract to the lowest bidder. Flexible displays operate under continuous physical tension. If a manufacturer shaves 25% off their quote, they are doing it by using cheap electro-deposited copper foil, low-flux magnets that slide out of position, or generic driver ICs that will begin flickering the moment your building heats up in the summer.
My practical recommendation is straightforward: write your engineering specifications around measurable component standards. Mandate 4-layer rolled-annealed copper FPC construction, specify N50 or higher neodymium magnets with mechanical fasteners, and require common-cathode power distribution to minimize heat buildup behind the curve.
Tie milestone payments strictly to performance: release the final 20% balance only after the fully assembled curved screen passes a continuous 72-hour full-load burn-in test on-site without dead pixels, seam lifting, or color drift. Crucially, require the manufacturer to provide an archived digital copy of the original factory optical calibration coefficients (.rcfgx or vendor equivalent) tagged to your production run's unique serial numbers. This way you can replace an accidental impact strike two years down the road, push the calibration data to the new spare module via software, and avoid an awkward, mismatched square in the middle of your curved display. Hope this helps you evaluate your vendor options with confidence.
For standard flexible modules utilizing multi-layer FPC boards, the reliable minimum bending radius typically ranges between 100mm and 150mm for P1.5mm to P2.5mm pixel pitches. Bending tighter than 100mm risks micro-fracturing the copper traces and popping diode solder joints. For large cylinders or sweeping waves with radii exceeding 500mm, standard flexible modules operate with zero mechanical strain.
Soft LED modules mount entirely via high-strength rear neodymium magnets that attach directly to a magnetically receptive curved sheet-metal or CNC-rolled steel substrate. The front of the module features tiny mechanical registration pins along its edges that lock into matching receiver holes on adjacent modules, maintaining alignment without visible faceplate screws.
Because soft modules are built on flexible polyimide substrates rather than rigid fiberglass, manual desoldering with a standard soldering iron carries a high risk of melting the thin substrate and damaging neighboring traces. On-site technicians do not replace individual diodes; instead, they use a specialized magnetic extraction tool to pop out the entire flexible module in under two minutes, swapping it with an identically binned spare module. The damaged unit is then sent back to the manufacturer for precision microscope rework.
Surface-Mount Device (SMD) packaging solders packaged diodes onto the flexible FPC; it is cost-effective and easy to produce, but individual diodes can be sheared off if the module is bent carelessly. Chip-on-Board (COB) bonds raw semiconductor dies directly to the flexible board and seals the entire face in a continuous layer of protective optical resin. Flexible COB provides vastly superior impact resistance, dust and moisture protection, and allows for even tighter bending radii, though it carries a 30% to 50% price premium over SMD.
For the United States and Canada, the equipment must hold an electrical safety listing under UL 62368-1 (or equivalent ETL certification) through an accredited NRTL, along with FCC Part 15 Class A or Class B electromagnetic compatibility verification. For the European Union, the hardware must carry valid CE markings backed by declarations of conformity for the Low Voltage Directive (LVD 2014/35/EU), EMC Directive (2014/30/EU), and full RoHS compliance.
Visible seams on a curved screen almost always result from minor mechanical variations in the underlying steel framework rather than defects in the LED modules themselves. If the curved steel backing has an irregular radius or surface burrs, the soft modules will follow those contours, causing adjacent edges to misalign. High-end video processors provide seam-brightness edge compensation features in software to help smooth out minor optical variations.
No. Flexible LED modules contain complex multi-layer electrical trace routing, internal power planes, and data shift registers throughout the entire board area. Attempting to cut or trim a module on-site will sever active circuits and permanently destroy the entire tile. All screen dimensions must be planned as exact multiples of the factory's standard modular dimensions (such as 240mm × 120mm, 320mm × 160mm, or 256mm × 128mm).
Enclosed structural columns require active internal ventilation. The core of the column must incorporate forced-air intake and exhaust ducting, or the display must be engineered using common-cathode power architecture. Common-cathode systems supply dedicated lower voltages (typically 2.8V to red diodes and 3.8V to green/blue diodes), reducing module heat generation by up to 30% compared to traditional 5V common-anode systems, allowing passive convection within the column.
Standard catalog flexible modules generally require 20 to 30 business days for automated SMT mounting, silicone molding, 72-hour burn-in testing, and optical calibration. If custom-engineered secondary sheet-metal frames or bespoke cabinet structures are included, production spans 35 to 45 business days. Ocean transit to West Coast US ports takes approximately 18 to 22 days, while transit to East Coast ports or Western Europe requires 30 to 40 days.
Flexible modules must never be packed loosely or stacked directly on top of each other. The purchase agreement must specify export-grade, non-fumigation plywood flight cases or wooden crates built to ISPM-15 standards. Each module must sit inside a precision-cut high-density EVA foam tray that supports the flexible backing without applying pressure to the front face diodes, sealed inside anti-static, moisture-barrier vacuum packaging with industrial desiccant packs.