English
If you need the direct, bottom-line verdict before going through the technical specifications: the global market for commercial indoor led display manufacturers divides into two distinct operational groups depending on your room architecture, service requirements, and capital budget. For mission-critical emergency command centers, broadcast news studios, and blue-chip corporate executive boardrooms where seven-figure budgets and guaranteed domestic on-site field support are mandatory, publicly traded enterprise giants such as Leyard (Planar), Unilumin, Absen, and Samsung (The Wall / IER series) provide turnkey peace of mind, audited UL 48 and ETL sign listings, and comprehensive regional service depots.
However, for roughly 85% of commercial installations—including corporate briefing centers, higher education lecture halls, worship sanctuaries, luxury retail flagships, and private conference suites—specialized Tier-2 export OEM and ODM engineering factories such as CreateLED, Dicolor, Gloshine, Uniview LED, AOTO, and Desay deliver virtually identical optical fidelity and mechanical precision at 35% to 50% lower capital expenditure. The non-negotiable rule when dealing with any supplier is to never purchase off an open-ended product catalog. You must contractually bind the internal Bill of Materials (BOM) to demand genuine gold-wire bonded LEDs (such as Nationstar RS or high-grade Kinglight), high-PWM constant-current driver ICs from Macroblock or Chipone, fanless Common Cathode power architecture, CNC-machined die-cast aluminum cabinets with under 0.05mm tolerances, and an on-site 5% pre-calibrated spare module package originating from the exact same diode manufacturing batch.
Now, let us examine how commercial indoor display manufacturing really works, where component downgrades hide, and how to configure a fine-pitch video wall that operates quietly and reliably for years to come.
Have you ever walked into a freshly commissioned corporate boardroom, looked up at an expansive 4K video wall that cost well over sixty thousand dollars, and noticed that several panel seams down the center look like hairline black fractures? Or worse, when the executive turns on a presentation with a dark slate background, the entire display turns into a noisy, mottled mess of reddish blotches and uneven grayscale banding, while a persistent electrical buzz hums quietly in the background.
This exact situation confronts commercial AV integrators, facility managers, and IT directors every single month. When you start reaching out to commercial indoor led display manufacturers, every vendor sends across glossy brochures claiming the exact same boilerplate specs: 800 nits of indoor brightness, 16-bit grayscale depth, a 3,840Hz refresh rate, seamless magnetic alignment, and a theoretical 100,000-hour operational lifespan. Yet one manufacturer quotes $1,600 per square meter, while another demands $5,200 for what seems to be the exact same 1.2mm pixel pitch.
Why does that pricing spread exist? Is the higher quotation just bloated corporate overhead, or does the budget option cut internal corners that will leave you with discolored modules and dead pixels after twelve months of daily meetings? When we are using these fine-pitch indoor screens under continuous commercial duty cycles, the difference between an industrial-grade installation and an unreliable assembly comes down to driver silicon architecture, circuit board copper thickness, chassis machining tolerances, and optical surface treatments. Let us look down together at what actually happens beneath the surface.
Commercial indoor displays operate under completely different physics than outdoor billboards. On an outdoor roadside pylon, displays blast 6,500 nits of raw light to fight direct solar glare, and viewers stand forty feet away. In an indoor boardroom, university auditorium, or control room, viewers sit between four and fifteen feet from the screen.
+--------------------------------------------------------------------------+
|                  INDOOR COMMERCIAL DISPLAY PRIORITIES                    |
+--------------------------------------------------------------------------+
|  [Low Operating Brightness] Must calibrate down to 100 - 300 nits        |
|  [Acoustic Silence]         Must operate at 0 dB (100% fanless)          |
|  [Ultra-Wide Viewing]       Color fidelity stable past 160 degrees       |
|  [Thermal Conduction]       Zero heat blasted into enclosed rooms        |
|  [Camera Compatibility]     Zero moiré & flicker during video calls      |
+--------------------------------------------------------------------------+
Because ambient indoor lighting typically sits around 300 to 500 lux, an indoor screen running at full brightness will blind meeting participants within ten minutes. That means an indoor commercial screen spends 90% of its operating life running at only 15% to 25% of its maximum brightness. If the manufacturer selected cheap driver chips, the image completely falls apart at those lower drive currents.
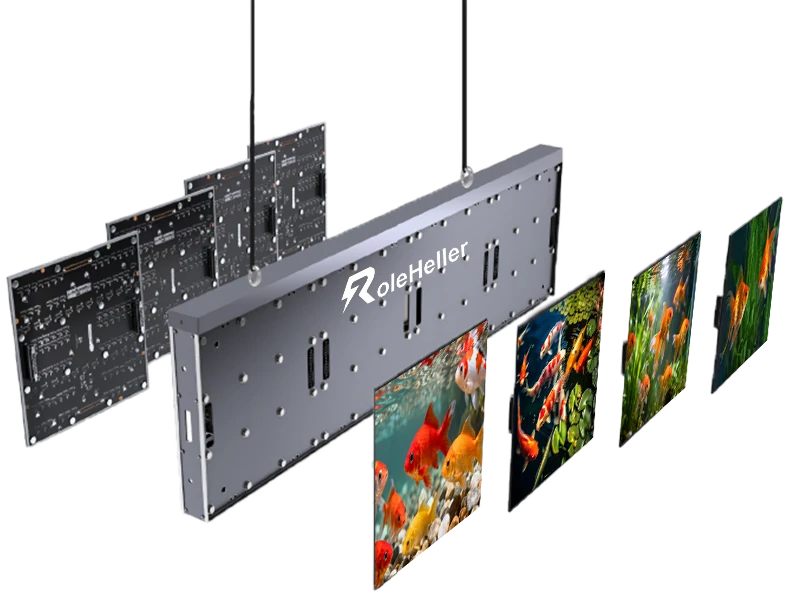
To evaluate commercial indoor led display manufacturers like an experienced hardware engineer, you have to look past the painted housing and inspect the internal Bill of Materials. A finished commercial indoor cabinet comprises five critical subsystems:
       +-------------------------------------------------------+
       |             FINE-PITCH INDOOR CABINET STACK           |
       +-------------------------------------------------------+
       | [Layer 1] Optical Face: SMD Diodes / GOB / COB Resin  |
       |-------------------------------------------------------|
       | [Layer 2] 6-to-8 Layer High-Tg FR4 PCB (2oz Copper)   |
       |-------------------------------------------------------|
       | [Layer 3] High-PWM Constant-Current Driver Silicon    |
       |-------------------------------------------------------|
       | [Layer 4] CNC Die-Cast Aluminum Chassis (±0.05mm)     |
       |-------------------------------------------------------|
       | [Layer 5] Dual-Rail Common Cathode Low-Noise PSU      |
       +-------------------------------------------------------+
Inside every surface-mount diode (SMD), hair-thin wires connect the microscopic semiconductor wafer to the outer electrical pins.
99.99% Pure Gold Wire Bonding: Top-tier manufacturers specify gold wire bonding (such as Nationstar RS series or Kinglight Gold-wire tier). Gold is chemically inert, handles thermal expansion without cracking, and provides stable electrical conductivity over years of operation.
Copper / Alloy Wire Bonding: Lower-cost assemblers frequently quote attractive prices by swapping in copper or copper-alloy wire. When trace moisture molecules penetrate the epoxy casing during humid summer months, copper oxidizes rapidly, leading to open-circuit failures and dead pixels across your display face.
The driver IC determines how cleanly the visual signal translates into light output, grayscale gradients, and camera capture stability.
High-Tier PWM Drivers (e.g., Macroblock MBI5359, MBI5264, or Chipone ICND2065): These feature 16-bit to 18-bit true grayscale processing, refresh rates from 3,840Hz to 7,680Hz, and dedicated hardware circuits to eliminate ghosting and dark lines. In dark conference rooms, shadows stay clean without shifting into noisy reddish or greenish tints.
Entry-Level Dual-Latch Drivers: Budget suppliers often configure screens using legacy ICs operating at 1,920Hz. While these look acceptable on static text, dimming the screen to comfortable meeting room levels causes severe color banding, and smartphone or PTZ video conference cameras capture harsh black scanning bars.
Indoor video walls operate in enclosed spaces where excess heat makes participants uncomfortable.
Traditional Common Anode: Both Red, Green, and Blue dice share a single 5.0V power rail. However, Red diodes only require approximately 2.1V to 2.4V to operate efficiently, while Blue and Green require roughly 3.2V to 3.8V. The excess voltage supplied to the Red diode is converted directly into wasted thermal energy, heating up the front surface of the display.
Common Cathode Design: Independent power lines feed the diodes with separate voltages (2.8V for Red, 3.8V for Green and Blue). This targeted power delivery reduces overall power consumption by 25% to 35%, lowers the working surface temperature of the cabinet by 8°C to 12°C, and prevents thermal color drift during long corporate presentations.
Choosing the right indoor display requires matching the diode packaging technology to your room usage and budget. Review this operational matrix before specifying your display:
| Packaging Technology | Native Pitch Range | Surface Impact Protection | Contrast & Black Depth | Field Repairability | Typical Cost Profile |
|---|---|---|---|---|---|
| Standard SMD | P1.2 – P2.5 | Low (Diodes exposed to physical impact) | Moderate (Matte black face masks) | Easy (Single-pixel hot-air rework) | Baseline 1.0x (Most Economical) |
| GOB (Glue-on-Board) | P1.2 – P1.8 | High (Transparent epoxy shield layer) | Good (Deep black epoxy finish) | Moderate (Requires specialized tools) | 1.15x – 1.30x |
| COB (Chip-on-Board) | P0.6 – P1.5 | High (Encapsulated wafer layer) | Exceptional (Seamless resin surface) | Challenging (Factory cleanroom return) | 1.40x – 1.80x |
| Micro LED (AM-TFT) | P0.4 – P0.9 | High (Direct active-matrix bond) | Reference Grade (Near-infinite contrast) | Tile-Swap Only (Cleanroom depot service) | 2.50x – 5.00+x |
If your display is installed in a high-traffic space—such as an interactive corporate lobby, university corridor, or church sanctuary where children, visitors, or cleaning crews can bump into the wall—standard SMD modules are vulnerable to having corner diodes knocked off. GOB applies a protective transparent polyurethane resin layer across the entire module face. This creates an impact-resistant, dust-tight surface that can be wiped clean with a microfiber cloth without damaging delicate solder joints.
When evaluating commercial indoor led display manufacturers, suppliers fall into distinct tiers based on production automation, technical agility, and warranty support:
+--------------------------------------------------------------------------+
|             COMMERCIAL INDOOR LED MANUFACTURING ECOSYSTEM                |
+--------------------------------------------------------------------------+
|  [TIER 1: Public Brand Leaders] Leyard/Planar, Unilumin, Absen, Samsung  |
|   -> Massive cleanroom automation, global field support, full UL listing |
|   -> Best for: Fortune 500 boardrooms, broadcast studios, civic command  |
|   -> Reality: 35% to 60% brand premium; slow to modify standard framing  |
|--------------------------------------------------------------------------|
|  [TIER 2: Export OEM/ODM Engineering Fabs] CreateLED, Dicolor, Gloshine, |
|           Uniview LED, AOTO, Desay                                       |
|   -> High-speed SMT lines, custom CAD agility, direct factory pricing    |
|   -> Best for: Corporate meeting rooms, higher education, retail flagships|
|   -> Reality: Exceptional build quality; requires strict BOM management  |
|--------------------------------------------------------------------------|
|  [TIER 3: Commodity Assemblers & White-Label Brokers]                    |
|   -> High-volume standard assembly, low unit prices, domestic focus      |
|   -> Best for: Short-term temporary displays, non-critical signs         |
|   -> Reality: Mixed diode bins, high heat, unreliable warranty coverage  |
+--------------------------------------------------------------------------+
Key Names: Leyard (Planar), Unilumin, Absen, Samsung Electronics, Sony.
The Operating Reality: These manufacturers operate sprawling automated cleanroom facilities with automated optical inspection (AOI) lines. They maintain regional repair centers and field engineers across North America and Western Europe.
The Trade-Off: Hardware pricing carries a significant brand premium. If your installation requires bespoke non-standard cabinet dimensions to fit inside existing architectural millwork, modifying their automated tooling lines can take months.
Key Names: CreateLED, Dicolor, Gloshine, Uniview LED, AOTO, Desay.
The Operating Reality: These facilities focus squarely on the international AV integration and corporate staging sectors. They run automated SMT lines equipped with Yamaha and Panasonic pick-and-place systems.
The Trade-Off: Sourcing managers must write precise technical specifications. Because Tier-2 plants offer multiple BOM configurations, leaving component details open allows factory sales desks to quote value-tier parts rather than their enterprise-grade packages.
Key Names: Unbranded white-label trading entities and low-cost domestic assemblers.
The Operating Reality: They produce standard plastic-backed modules using low-grade copper-wire LEDs, generic driver chips, and basic power supplies.
The Risk: Inconsistent diode binning leads to noticeable checkerboard color patches. Heat dissipation is poor, leading to premature diode failure and dropped scan lines within twelve to eighteen months.
| Technical Parameter | Tier-1 Enterprise Giants | Tier-2 Engineering OEM/ODM | Tier-3 Budget Assemblers |
|---|---|---|---|
| Typical Cost (P1.25 per m²) | $3,500 – $6,500+ USD | $1,800 – $2,800 USD | $900 – $1,300 USD |
| Primary LED Packaging | Nationstar Gold Wire / Nichia / Cree | Nationstar Gold or Copper / Kinglight | Generic Brand / Alloy Wire |
| Driver Silicon Standard | Macroblock MBI5359 / Chipone 2065 | Chipone ICND2153 / Macroblock 5153 | Unbranded Dual-Latch ICs |
| Refresh Rate | 3,840Hz – 7,680Hz | 3,840Hz | 1,920Hz |
| Cabinet Construction | CNC Die-Cast Magnesium / Aluminum | Die-Cast Aluminum Profile | Stamped Sheet Metal / Iron |
| Dimensional Tolerance | ≤ 0.05 mm (Zero visible seam) | ≤ 0.1 mm | ≥ 0.5 mm (Visible panel gaps) |
| Power Architecture | Common Cathode Energy-Saving Standard | Common Cathode or Hybrid High-Eff | Traditional 5.0V Common Anode |
| Certification Level | Full UL 48, ETL, FCC Class B, CE-EMC | Genuine ETL / UL / CE-EMC Listed | Self-declared CE marks only |
| Calibration Architecture | Pixel-by-pixel chromatic & luma files | Full-panel bin calibration archive | Uncalibrated / factory default |
| Expected Service Life | 80,000 to 100,000 Hours (Stable) | 60,000 to 80,000 Hours | 20,000 to 35,000 Hours |
One common mistake commercial buyers make when liaising with commercial indoor led display manufacturers is neglecting physical maintenance access until the structural framing is already bolted to the conference room wall.
FRONT ACCESS (Modern Corporate Setup)   REAR ACCESS (Legacy Catwalk Setup)
+------------------------+              +------------------------+
| [Module] <== Vacuum    |              | [Module]     | Catwalk |
| [Chassis Frame]        |              | [Cabinet]    | Space   |
| [Drywall or Stud Wall] |              | [Rear Door] <| Corridor|
+------------------------+              +------------------------+
(Needs 0mm rear clearance)              (Requires 700mm-900mm rear space)
Front-Service Systems: The LED modules are held firmly against the die-cast cabinet chassis using high-strength neodymium magnets. When a module experiences an issue, a technician stands directly in front of the screen, engages an electric vacuum-suction extraction tool, and releases the module in seconds. Power supplies and receiving cards are immediately accessible through the front opening. This setup lets you mount the entire display flush against an existing drywall or executive wood-paneled wall with zero rear clearance, saving valuable office floor space.
Rear-Service Systems: Cabinets feature hinged metal doors on the back. To service a power unit or receiving card, a technician must physically walk behind the screen. If your installation site does not have a dedicated 30-inch maintenance corridor behind the wall, you cannot use a rear-service cabinet.
When presenting an investment proposal to corporate stakeholders or property managers, looking solely at the purchase invoice is a recipe for budget surprises. An indoor screen running 12 to 14 hours per day generates thermal wattage that your building HVAC system must remove.
"An indoor video wall running traditional Common Anode architecture functions like a three-kilowatt electric space heater mounted to your boardroom wall. Within forty-five minutes of closing the meeting room doors, the ambient temperature rises noticeably, forcing the building air conditioning into overdrive and wasting substantial commercial power."
Let us run a real-world calculation comparing a standard Common Anode display against a modern Common Cathode display across a standard 15-square-meter boardroom video wall (roughly 17 feet wide by 9.5 feet high):
[Traditional Common Anode Screen (15m²)]
Average Power Consumption: ~320W per m²
Hourly Consumption: 4.8 kW
Daily Consumption (12 hours): 57.6 kWh
Annual Heat Generated: ~59,000 BTU/hr peak thermal load
Five-Year Operating Energy: ~$37,843 USD (@ $0.18/kWh)

[Modern Common Cathode Screen (15m²)]
Average Power Consumption: ~200W per m²
Hourly Consumption: 3.0 kW
Daily Consumption (12 hours): 36.0 kWh
Annual Heat Generated: ~36,000 BTU/hr peak thermal load
Five-Year Operating Energy: ~$23,652 USD (@ $0.18/kWh)
By mandating Common Cathode technology from your manufacturer, you save over $14,000 in electricity alone over a five-year lifecycle on a modest boardroom screen. Even better, the display surface remains cool to the touch, and your meeting participants will not break into a sweat during executive presentations.
When your crated display hardware arrives on site, precise physical alignment makes the difference between a pristine, seamless canvas and an eyesore.
                  SIX-STEP COMMISSIONING PROTOCOL

[Step 1: Structural Laser Leveling]  ===> Shoot rotary laser across foundation rail
                 |
[Step 2: Base Cabinet Rigging]       ===> Mount master center row; lock eccentric bolts
                 |
[Step 3: Signal Loop Daisy-Chain]    ===> Primary Ethernet + Redundant Return Loop
                 |
[Step 4: Common Cathode Power Bus]   ===> Balanced single-phase or 3-phase AC wiring
                 |
[Step 5: Front-Magnetic Tile Snap]   ===> Center-out placement using vacuum tool
                 |
[Step 6: Optical Seam Calibration]   ===> Camera-assisted coefficient profiling
Follow this sequential engineering procedure:
Level the Structural Foundation Bar: Before hanging any cabinets, level your bottom horizontal mounting rail using a precision rotary laser level. If the baseline steel is unlevel by even 0.5mm across a four-meter span, that error will compound into severe panel overlap and visible seam gaps at the upper corners.
Anchor Cabinets from the Center Outward: Bolt the center cabinets of your bottom row to the structural frame first, working outward toward the perimeters. Use the built-in precision alignment pins and adjust mechanical eccentric bolts to eliminate seam gaps before tightening structural anchors. That way, you can easily guarantee a razor-flat front plane across the entire active display.
Route Signal Loops with Hardware Redundancy: Run your primary Gigabit Ethernet signal line from port 1 of your master video processor (such as a NovaStar COEX MX40 Pro or Colorlight Z6 PRO) into the bottom-left cabinet, daisy-chaining across the wall. Then, run a backup return line from the final cabinet back to the processor's redundant port. If an intermediate network cable fails, the backup loop engages instantly without dropping video frames.
Distribute AC Power Evenly Across Circuits: Calculate total cabinet current draw and split electrical circuits evenly across available breakers to prevent neutral-line overheating. Ensure dedicated ground cables bond directly from the cabinet chassis to the building electrical ground with a resistance reading under 4 ohms.
Mount Magnetic Modules from Center Outward: Use an electric vacuum-suction extraction tool to place magnetic modules onto cabinet chassis plates. Starting in the center and moving outward prevents accumulated physical tension across module edges. Never slide modules against each other; seat them directly forward to avoid chipping fragile corner diodes.
Execute Camera-Assisted Seam Calibration: After powering on the display and allowing it to reach thermal equilibrium (around 45 minutes), use a DSLR calibration camera kit paired with NovaStar NovaLCT or Colorlight software to capture optical seam boundaries. The software detects micro-brightness variations at cabinet joints and applies localized edge-correction coefficients, producing a uniform visual canvas.
To help you navigate technical reviews during vendor negotiations, let us tackle the toughest practical questions that commercial AV professionals encounter:
Moiré occurs when the physical grid pattern of individual LED diodes interferes with the pixel sensor grid of a digital camera. This optical interference creates distracting, wavy, rainbow-like artifacts across video recordings and Zoom/Teams calls.
How to solve this:
Optical Diffusion Coatings: Choose GOB or COB modules treated with matte, anti-reflective micro-bead coatings that soften diode point-source edges.
Optical Anti-Moiré Filters: Apply a specialized resin film across the screen surface to blend adjacent light cones before camera sensors register them.
Camera Configuration: Adjust camera distance, focal length, and aperture to slightly defocus the LED plane while keeping on-camera presenters in sharp focus.
Most commercial LED screens look vivid when displaying full white or high-saturation primary colors. The real test occurs when displaying subtle shadows, dark gradients, or soft facial tones at low brightness levels (10% to 15% of peak output).
Cheaper driver ICs drop from 16-bit processing down to 10-bit or 8-bit depth at low drive currents, causing visible stepping rings, color banding, and red tint shifts in dark backgrounds.
To prevent this flaw, mandate driver ICs featuring Low-Grayscale Calibration and High-PWM bit depth (such as Macroblock MBI5359 or Chipone ICND2065). These driver chips maintain full 16-bit grayscale depth down to 0.05 nits, ensuring smooth tonal gradations in darkened viewing rooms.
If you are running a standard SMD or GOB display, on-site repairs are straightforward.
A technician uses a vacuum extraction tool to pop out the defective module, swaps in a factory-calibrated spare module from your on-site spare cache in under two minutes, and sends the damaged module to a local repair depot. Specialized technicians can desolder and replace individual surface-mount diodes using a micro-hot-air station.
However, if you are running a COB display where diodes are sealed under a continuous resin sheet, individual diode rework cannot be done on a field bench; the module must be returned to the manufacturer's cleanroom facility for precision laser repair.
Never wire a 30% initial deposit based solely on a PDF presentation and a polished website. If you are ordering a sizable commercial project, follow this four-point testing protocol during your pre-shipment factory audit:
+--------------------------------------------------------------------------+
|                  PRE-SHIPMENT FACTORY AUDIT PROTOCOL                     |
+--------------------------------------------------------------------------+
|  [ ] 1. Continuous 72-Hour Burn-In Testing                               |
|      - 24 hours full white balance at 100% brightness                    |
|      - 24 hours alternating pure Red, Green, and Blue test patterns      |
|      - 24 hours high-motion dynamic video playback                       |
|--------------------------------------------------------------------------|
|  [ ] 2. Low-Brightness Grayscale Verification                            |
|      - Dim screen to 5% brightness; display a 15% gray raster pattern    |
|      - Inspect for horizontal banding, red tint shifts, or dead pixels   |
|--------------------------------------------------------------------------|
|  [ ] 3. Camera Shutter Diagnostic Scan                                   |
|      - Film active screen using a DSLR at 1/1000s and 1/2000s shutter    |
|      - Confirm complete absence of black scan bars and flickering        |
|--------------------------------------------------------------------------|
|  [ ] 4. Acoustic Noise Verification                                      |
|      - Measure decibel levels at 1 meter from active display rear        |
|      - Must register below 20 dB (completely inaudible in meeting rooms) |
+--------------------------------------------------------------------------+
When reviewing video verification of your assembled display during burn-in testing, watch the screen when a solid white image is shown. A pure white raster reveals everything: if individual cabinets display subtle variations in color temperature—some leaning warm pink, others cool blue—the factory has mixed different diode binning batches. Reject that configuration immediately; every module on your screen must originate from the exact same diode wavelength and luminous intensity bin.
Having spent years evaluating display hardware, tearing down failed modules, and walking factory cleanrooms across Shenzhen and Huizhou, here is my honest take: you do not need to pay a 60% brand premium to corporate conglomerates to get a breathtaking, highly reliable indoor video wall. But you absolutely cannot treat commercial indoor LED displays like an off-the-shelf consumer television purchase where you simply pick the cheapest bid on an import platform.
The real risk when buying from overseas manufacturers is rarely intentional malice; it is almost always ambiguity. When an inexperienced buyer simply submits an inquiry asking for "the best price on an indoor P1.25 4K video wall," the factory sales clerk assumes the client is looking for the lowest possible bid to win a low-cost tender. They will quote thin 2-layer circuit boards, copper-wire diodes, basic driver chips, and noisy generic power supplies because they assume price is the only metric that matters to you.
If you change the conversation from your very first email by sending an explicit, highly detailed technical specification:
Mandating 6-to-8 layer FR4 PCBs with 2oz copper planes.
Specifying Nationstar Gold-wire or Kinglight Gold-tier diodes.
Requiring Macroblock or Chipone high-PWM driver silicon.
Demanding CNC die-cast aluminum or magnesium alloy cabinets with ≤ 0.05 mm seam tolerances.
Requiring a 5% pre-calibrated spare module package from the master production run.
The manufacturer immediately recognizes your technical expectations. They will bypass the junior sales desk and route your project directly to their senior engineering team. That ensures you receive industrial-grade display hardware that installs smoothly, operates quietly, and delivers crystal-clear presentations for years to come. Hope this helps you out on your next deployment!
For standard corporate boardrooms and conference suites where viewers sit between 5 and 12 feet (1.5 to 3.5 meters) from the display, the optimal pixel pitch is P1.25mm to P1.56mm. At these pitches, a standard 130-inch to 165-inch diagonal video wall delivers native 1080p or 4K UHD resolutions with zero visible pixel structure to viewers seated around the conference table.
Commercial indoor fine-pitch LED video walls generally range from $1,800 to $3,500 USD per square meter for high-quality Tier-2 engineering OEM/ODM hardware (such as P1.25 or P1.56 pitches with Nationstar gold-wire LEDs and Macroblock ICs). Top-tier enterprise brands like Leyard, Absen, or Samsung range from $4,000 to $7,500+ USD per square meter, while budget commodity assemblers quote between $1,000 and $1,400 USD per square meter.
SMD solders individually packaged LED diodes directly onto the front surface of the PCB, using plastic louvers for mechanical protection. COB mounts bare semiconductor micro-wafers directly onto the board substrate, sealing the entire module surface under a continuous, protective optical resin layer. COB provides superior impact resistance, ultra-wide 170-degree viewing angles, and deeper black levels, but individual diode field repairs must be handled at dedicated cleanroom repair centers.
Common Cathode architecture routes separate, dedicated DC voltage lines to the Red diodes (2.8V) and Green/Blue diodes (3.8V), rather than supplying a uniform 5.0V shared rail. Because Red diodes do not have to burn off excess voltage as waste heat, overall power consumption drops by 25% to 35% and surface temperatures decrease by 8°C to 12°C. This lower thermal load keeps meeting spaces comfortable and eliminates the need for loud cooling fans.
For installations in the United States and Canada, the entire assembled display system must carry an authentic UL 48 (Standard for Electric Signs) or ETL equivalent listing, along with FCC Part 15 Class B electromagnetic compliance for commercial office buildings. For the European Union, the display must carry certified CE-EMC, CE-LVD, and RoHS compliance reports issued by recognized testing bodies.
Yes. Modern fine-pitch indoor displays feature 100% front-serviceable architectures. LED modules are held firmly against the cabinet chassis by high-strength neodymium magnets. Technicians use an electric vacuum-suction extraction tool placed against the module face to safely pull panels forward, providing access to internal receiving cards, flat ribbon cables, and power supplies without requiring rear access corridors.
Your purchase contract should mandate an on-site spare parts package of at least 5% spare LED modules, 5% spare power supplies, 2% to 3% spare receiving cards, along with replacement ribbon data cables, magnetic extraction tools, and proprietary cabinet alignment hardware. Crucially, all spare modules must originate from the exact same diode production batch to ensure matching color temperature and luminance characteristics.
A commercial fine-pitch LED display built with gold-wire diodes and brand-name driver silicon has an expected operational lifespan of 80,000 to 100,000 hours (roughly 9 to 11 years of 24/7 operation) before brightness decays to 50% of its initial value. Running displays at moderate brightness levels (150 to 300 nits) in climate-controlled spaces prevents thermal stress and extends component lifespan.
The global market is led by NovaStar (using their COEX platform with MX-series processors and Armor/A10s Pro receiving cards) and Colorlight (using Z-series processors and 5G receiving cards). These platforms support low-latency 4K/8K video processing, 16-bit to 22-bit grayscale depth, HDR10/HLG color profiles, and automated camera-based seam calibration.
For standard die-cast aluminum cabinets using established pixel pitches (such as P1.25, P1.56, or P1.87), factory production generally takes 20 to 30 business days, which includes the mandatory 72-hour continuous burn-in testing cycle. Bespoke curved frames, custom architectural cabinet dimensions, or specialized high-density COB configurations typically require 35 to 50 business days for tooling and validation.