English
If you need an immediate, field-proven answer on how to select wholesale led display screen manufacturers without burning your commercial budget or dealing with catastrophic module failures, here is the direct benchmark: partner strictly with direct assembly manufacturers that build with verified gold-wire bonded LEDs (Nationstar or Kinglight high-spec), paired with constant-current pulse-width modulation (PWM) driver ICs delivering at least 3,840 Hz refresh rates (Macroblock MBI5153 or Chipone ICN2053), CNC-machined die-cast aluminum cabinets with edge tolerances under 0.05 mm, and certified power supplies featuring active power factor correction (Mean Well UHP or Great Wall with PFC > 0.95). Furthermore, you must contractually mandate a continuous 72-hour full-white burn-in test on the factory floor and insist on a batch-matched single-bin 5% spare module allotment drawn from the exact same diode wafer lot. If an overseas supplier dodges your request for unedited video documentation of their automated surface-mount lines or cannot produce verifiable UL 48, UL 8750, or CE full-assembly safety listings, walk away immediately—no matter how cheap their square-meter pricing looks on paper.
Picture this realistic scenario: you run a commercial audio-visual integration firm, an electrical contracting business, or a digital out-of-home (DOOH) advertising agency in Dallas, Rotterdam, or Chicago. You just secured a major contract to deliver a 300-square-meter outdoor roadside digital billboard along an interstate, a fine-pitch P1.5 video wall for an executive boardroom, and a curved staging screen for a premier event center. You jump online to source from wholesale led display screen manufacturers, and within twenty-four hours your inbox is flooded with fifty different product catalogs. The quotes vary wildly from $280 to $1,400 per square meter. Every factory sales rep swears that their facility is the top manufacturer in Shenzhen or Huizhou, their diodes are Grade A, and their warranty covers you for five years.
What happens when your procurement team picks a lowball vendor, wires the deposit, and waits out ocean freight? The shipping containers arrive at your warehouse, your rigging crew hoists the cabinets thirty feet up onto a roadside steel structure, and problems start cascading. When your master electrician opens the primary power junction box, the local municipal building inspector red-tags the job site because the sign assembly lacks an authentic UL 48 or ETL certification sticker. Two months later, driving winter sleet and freezing rain penetrate cheap perimeter rubber gaskets, moisture wicks into the flat ribbon cables, and four horizontal rows of modules go completely black. Renting a boom truck at $1,500 a day to swap modules in freezing winds eats up your entire project margin in forty-eight hours, while the overseas sales rep suddenly stops replying to your messages.
When we are installing commercial digital screens, saving a few dollars on the initial invoice is never worth the nightmare of field downtime. Some folks want the lowest upfront price, but what should you do when maintenance costs start piling up? Let's dive right in and walk through the engineering physics, component grades, factory auditing protocols, and contracting rules you need to secure hardware that runs reliably for a decade.
When we install a stationary digital display or roadside electronic message center, that hardware operates in an open-air battleground. Unlike an indoor television panel that sits in a climate-controlled room, an exterior commercial screen sits exposed to hostile environmental forces twenty-four hours a day, year in and year out.
[Direct Solar Radiation (80,000+ Lux & 50°C Ambient)] ──► Severe Thermal Stress & Diode Degradation
[Freezing Sleet & Sub-Zero Winter Winds (-30°C)]      ──► PCB Contraction & Solder Joint Cracking
[Airborne Salt Fog, Dust & Diesel Particulates]       ──► Copper Trace Corrosion & Gasket Decay
[High-Velocity Wind Shear & Structural Vibration]     ──► Cabinet Deflection & Ribbon Disconnects
Severe Thermal Cycling: The cabinet structure must expand and contract smoothly across temperature swings ranging from -35°C during a Midwestern blizzard to +50°C under direct summer sunshine in Texas or southern Spain.
Solar Radiation and UV Degradation: Inexpensive plastic module masks and low-grade silicone potting dry out, turn chalky, and warp under solar ultraviolet light, creating glare and micro-fissures that draw in rainwater through capillary action.
Corrosive Moisture and Internal Condensation: Rapid temperature drops at dusk cause warm, humid daytime air to condense into liquid water inside a metal cabinet. If the internal circuit boards lack thick conformal coating and breathable waterproof membrane vents, droplets form on live 5V electrical rails, triggering short circuits.
"According to International Electrotechnical Commission (IEC 60529) and National Electrical Code (NEC Article 600) engineering mandates, exterior digital signage enclosures must maintain continuous internal pressure equilibrium. An unventilated sign enclosure in full sun can experience internal ambient temperatures 25°C higher than the surrounding outdoor air, accelerating diode lumen decay by up to 300% if thermal pathways are inadequate."
A roadside digital sign is fundamentally an industrial electrical appliance. When viewers are passing by at 60 mph, readability depends entirely on optical contrast and stable lumen output, not paper-thin smartphone bezels. A high-contrast P8 or P10 display with deep-profile matte-black louvers and single-bin color diodes will outshine and outlast a cheap, washed-out P4 display every single day.
[Viewing Distance vs. Pixel Pitch Acuity Formula]
Minimum Comfortable Viewing Distance (MVD in meters) ≈ Pixel Pitch (in mm) × 1.0 to 1.5
For P8 Outdoor: 8.0 mm × 1.0 = 8.0 meters (approx. 26 feet)
For P2.5 Indoor: 2.5 mm × 1.0 = 2.5 meters (approx. 8 feet)
Picking the wrong pixel pitch or luminance spec is one of the fastest ways to burn through a project budget. Finer pixel pitch gives higher resolution, but it costs significantly more, generates more heat, and yields diminishing returns when viewers are sitting two hundred feet away in highway traffic.
The reference matrix below details typical engineering benchmarks across successful commercial installations:
| Application Category | Optimal Pixel Pitch | Calibrated Output (Nits) | Optimal Viewing Range | Ingress Protection (IP) | Primary Commercial Use |
|---|---|---|---|---|---|
| Indoor Boardroom / Conference | P0.9 – P1.56 mm | 600 – 1,000 | 3 to 20 ft (1 – 6 m) | IP40 (Front service) | Corporate boardrooms, command centers, luxury retail displays |
| Worship Sanctuary / Auditorium | P2.0 – P3.9 mm | 800 – 1,500 | 10 to 60 ft (3 – 18 m) | IP40 / GOB coated | Church stage backdrops, university halls, indoor arenas |
| Outdoor Commercial Monument | P6.0 – P8.0 mm | 6,500 – 7,500 | 20 to 120 ft (6 – 36 m) | IP65 Front / IP54 Rear | Bank roadside pylons, auto dealerships, school marquees |
| Highway Digital Billboard | P10 – P16 mm | 7,500 – 9,500+ | 35 to 400 ft (10 – 120 m) | IP65 Front / IP65 Rear | Interstate advertising structures, commercial truck stop towers |
| Sports Arena Perimeter & Score | P4.0 – P8.0 mm | 6,000 – 7,500 | 15 to 150 ft (5 – 45 m) | IP65 / Soft rubber mask | Stadium ribbon displays, foul pole timers, perimeter boards |
| Architectural Media Façade | P16 – P31.25 Mesh | 6,500 – 8,500 | 80 to 600 ft (25 – 180 m) | IP67 Wind-permeable | Glass skyscraper wrappers, stadium exterior media bands |
When sourcing from wholesale led display screen manufacturers, the packaging method is the single biggest factor governing visual contrast, physical durability, and long-term diode survival.
[Traditional SMD 1515/2121]          [GOB Polyurethane Shield]          [Flip-Chip COB Matrix]
┌─────────────────────────┐         ┌─────────────────────────┐        ┌─────────────────────────┐
│ Exposed pins & wire weld│         │ Encapsulated epoxy fill │        │ Direct die on substrate │
│ Vulnerable to physical  │         │ Impact and water proof  │        │ Ultra-deep black level  │
│ impact and humidity     │         │ High mechanical barrier │        │ Zero wire bond failure  │
└─────────────────────────┘         └─────────────────────────┘        └─────────────────────────┘
Standard SMD packages (such as SMD 1515, 2121, or 2727) use individual plastic leaded chip carriers containing three color dies soldered to the printed circuit board.
The Good: Highly economical, mature color-matching capabilities across production lots, and easily repaired on an electronics bench using a standard hot-air rework station.
The Bad: Diodes sit raised above the circuit board surface without physical shielding. A slight bump during installation or cleaning will shear diodes off the edge of a tile. Exposed copper pins are also vulnerable to moisture oxidation and sulfur corrosion in humid climates.
GOB takes a populated SMD circuit board and pours an optically clear polyurethane or epoxy shield across the entire front face, filling all gaps between diodes.
The Good: Outstanding impact resistance. You can strike the surface with a tool, wipe it down with cleaning solvents, and install it in high-traffic commercial corridors without worrying about passersby picking off pixels. It delivers an IP65 mechanical barrier against dust and liquids.
The Bad: The resin adds thermal resistance, trapping heat around the driver ICs if the PCB lacks adequate copper thermal vias. If the factory uses cheap industrial resin, the surface turns yellow after two years of indoor lighting exposure, destroying your white balance.
Instead of packaging the red, green, and blue semiconductor dies into individual plastic housings with tiny bonding wires, COB mounts bare micro-LED dies directly onto the PCB substrate face-down, sealed beneath an integrated resin layer.
The Good: Flip-chip architecture removes bonding wires entirely, eliminating the primary point of physical and thermal failure. It provides deep black backgrounds, contrast ratios exceeding 20,000:1, wide 170-degree viewing angles without color shift, and superior thermal conductivity through the board.
The Bad: Wholesale pricing is roughly 35% to 50% higher than standard SMD. More critically, on-site field repairs of single pixels are impossible; damaged modules must be sent back to the factory for specialized cleanroom laser micro-rework.
Inside every surface-mount LED diode, a microscopic wire connects the semiconductor die to the lead frame.
99.99% Pure Gold Wire Bonding: Gold never oxidizes. It flexes smoothly during rapid thermal expansion cycles and maintains low forward-voltage resistance across tens of thousands of runtime hours. Reputable assemblers use Nationstar Gold Wire series or genuine Cree/Nichia packages.
Copper or Composite Alloy Wire: Discount workshops slash 20% to 30% off diode costs by substituting copper or composite alloy wire. When microscopic atmospheric moisture penetrates the epoxy lens, copper oxidizes rapidly. Over months of thermal cycling, mismatched expansion rates break the bond welds, causing dead pixels to spread across your screen. Always insist on written contract clauses specifying gold-wire packaging.
Heat is the absolute enemy of digital screens. In traditional common-anode architecture, a single 5V or 4.2V power rail feeds red, green, and blue semiconductor dies simultaneously.
The electrical physics breakdown:
Blue and green LED dies need roughly 2.8V to 3.2V to emit light.
Red dies require only 1.8V to 2.1V.
In a common-anode circuit, that extra 1.0V to 1.3V pumped into the red diode turns directly into heat.
Multiply that waste across millions of pixels, and a large display wall dumps massive amounts of radiant heat into the room or enclosure. The screen surface heats up, cooking internal solder points, causing localized color drift, and stressing power supplies.
[Common-Anode Circuit: High Thermal Loss]
5.0V Power Rail ──► Red Diode (Draws 2.0V) ──► 3.0V Wasted as Pure Heat!
                ──► Green Diode (Draws 3.0V) ──► 2.0V Wasted
                ──► Blue Diode (Draws 3.0V)  ──► 2.0V Wasted

[Common-Cathode Circuit: Cool-Running & Efficient]
Rail A (1.8V) ──► Red Diode   ──► Minimal Waste Heat
Rail B (2.8V) ──► Green Diode ──► Optimal Efficiency
Rail C (2.8V) ──► Blue Diode  ──► Optimal Efficiency
This is why top-tier wholesale led display screen manufacturers mandate Common-Cathode architecture. By separating the electrical rails—feeding an independent 1.8V to red diodes and 2.8V to blue and green—overall panel power consumption drops by 25% to 40%. The internal cabinet runs 10°C to 15°C cooler, extending component lifespans by years and allowing the use of fanless, dead-silent power supplies.
When you compare quotes across different factories, understanding the raw manufacturing bill of materials (BOM) helps you distinguish genuine volume value from dangerous cost-cutting.
┌───────────────────────────────────────────────────────────┐
│ Typical Commercial LED Display Bill of Materials Breakdown│
├───────────────────────────────┬───────────────────────────┤
│ LED Diodes (R, G, B Packages) │ 35% - 42% of total cost   │
│ Constant-Current Driver ICs   │ 16% - 22% of total cost   │
│ CNC Die-Cast Cabinet Chassis  │ 14% - 18% of total cost   │
│ Multilayer PCB (4-6 Layer)    │ 12% - 16% of total cost   │
│ Power Supplies (Mean Well)    │ 8%  - 12% of total cost   │
│ Receiving Cards & Cabling     │ 5%  - 8%  of total cost   │
│ SMT Production & 72h QA Burn  │ 6%  - 10% of total cost   │
└───────────────────────────────────────────────────────────┘
The table below illustrates what you actually receive across different market price brackets:
| Engineering Component | Cut-Rate Low-End Spec | Standard Commercial Spec | Enterprise Infrastructure Spec |
|---|---|---|---|
| Wholesale Price (P8/P10) | $280 – $380 / m² | $480 – $750 / m² | $850 – $1,400+ / m² |
| Diode Wire Bonding | Unbranded copper/alloy wire | Kinglight / Nationstar copper | Nationstar Gold / Cree / Nichia |
| Driver IC & Refresh | Basic dual-latch, 960 – 1,920 Hz | Chipone ICN2053, 3,840 Hz | Macroblock MBI5359, 7,680 Hz |
| Power Supply Units | Unbranded generic 5V, no PFC | Chuanglian or Megmeet standard | Mean Well UHP slimline (Active PFC > 0.95) |
| Cabinet Construction | Thin sheet iron, manual spray paint | 1.5mm cold-rolled steel, powder coat | Marine 6063-T6 CNC aluminum (IP65) |
| Waterproofing Potting | Low-grade oil-filled silicone | Standard two-part polyurethane | Optical-grade silicone + Gore-Tex vents |
| Controller Architecture | Basic USB/Wi-Fi unbranded card | NovaStar TB-series cloud gateway | Dual-loop redundant NovaStar / Colorlight |
| Electrical Certification | Self-declared "CE" sticker only | Component-level UL power supply | Full-Cabinet UL 48 / ETL / CE listed |
| Year-One Failure Rate | Over 50 PPM (Frequent service) | Under 15 PPM (Manageable) | Under 3 PPM (Near zero) |
When you are sending tens or hundreds of thousands of dollars overseas, you cannot rely on trust alone. You need an uncompromising factory acceptance testing (FAT) protocol before releasing your final balance payment.
[Freeze Exact BOM in Sales Contract]
                 │
                 ▼
[SMT Automated Placement & 3D SPI Inspection]
                 │
                 ▼
[High-Pressure Water Chamber Spray Test (IP65)]
                 │
                 ▼
[72-Hour Continuous Full-Load White Burn-in Marathon]
                 │
                 ▼
[Thermal Imaging Scan for Hot Driver ICs & Power Terminals]
                 │
                 ▼
[Chroma & Luma Camera Calibration -> Wooden Crate Packing]
Lock down the exact bill of materials in writing before wiring your deposit. Never accept vague catalog descriptions like "High Quality Commercial LED Display." Your purchase contract must specify:
Diode package: Nationstar Gold-Wire SMD2727 (outdoor) or SMD1515/2121 Black Face (indoor), single-bin sorting lot.
Driver IC: Macroblock MBI5153 or Chipone ICN2053 delivering verified 3,840 Hz refresh rate and 16-bit grayscale.
Power supply: Original Mean Well UHP series fanless with active Power Factor Correction (PFC > 0.95).
Cabinet chassis: Precision die-cast aluminum alloy, magnetic front service, verified tolerance within ±0.05 mm.
Ingress protection: Certified IP65 front and rear with automated two-part silicone potting and Gore-Tex breathable membrane vents.
Walk the surface-mount technology (SMT) floor or hire an independent inspection agency to verify their equipment.
Ensure bare LED reels are stored inside climate-controlled dehumidification dry-cabinets. If diodes absorb ambient atmospheric moisture prior to reflow soldering, that moisture vaporizes into high-pressure steam inside the reflow oven, creating microscopic internal delamination (the classic "popcorn effect") that causes premature diode death in the field.
Verify that the factory runs automated 3D Solder Paste Inspection (SPI) before chip placement, followed by a multi-zone nitrogen reflow oven and 100% 3D Automated Optical Inspection (AOI) to catch solder bridging and cold solder joints before silicone potting is applied.
Demand unedited video proof of an actual water test.
The factory must mount sample modules into a finished cabinet and spray them in a testing chamber using high-pressure oscillating water jets from every angle for at least thirty minutes.
Right after the spray-down, technicians must unlatch the modules and demonstrate zero water ingress behind the perimeter silicone gaskets and cable gland entries.
Early electronic failure follows the classic bathtub curve: if a capacitor, diode, or driver IC has a manufacturing defect, it will almost certainly fail within the first 48 to 72 hours of electrical stress.
The factory must wire the entire display order together on test racks and run an uninterrupted 72-hour burn-in cycle.
This must include: 24 hours of full-raster white screen at 100% brightness (stressing power supplies and thermal dissipation), 24 hours of alternating primary RGB patterns (catching dead sub-pixels), and 24 hours of dynamic, high-contrast video loop testing.
During the full-white burn-in test, have an inspector walk the line with a calibrated thermal imaging camera. If any driver IC or power terminal spikes above 70°C in an ambient 25°C room, the thermal design is inadequate and requires correction.
Before dismantling the display array for crating, the manufacturer must run full-screen camera-based pixel-level calibration (chroma and luma calibration). A high-resolution CCD calibration camera captures the optical output of every single diode across the screen, calculates correcting coefficient matrices for red, green, and blue, and flashes those calibration values directly into the onboard EEPROM memory of each receiving card. This eliminates subtle batch color variances and ensures seamless edge blending across modular boundaries.
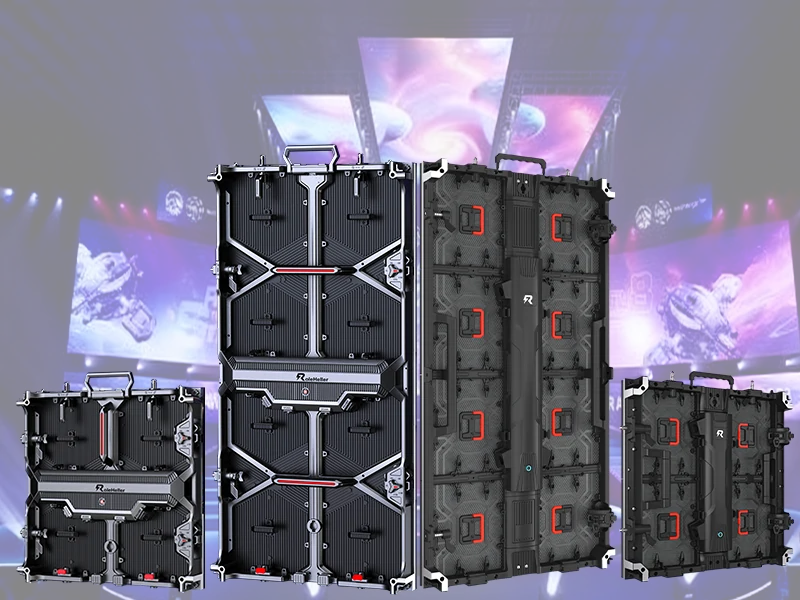
When sourcing commercial displays, you must evaluate the physical cabinet housing. How the modular tiles are mechanically supported determines whether your wall will assemble as an optically seamless plane or a patchwork of visible gaps.
[Standard 960mm × 960mm Cabinet Modular Grid]
┌───────────────────┬───────────────────┐
│ Module (480×480)  │ Module (480×480)  │
├───────────────────┼───────────────────┤
│ Module (480×480)  │ Module (480×480)  │
└───────────────────┴───────────────────┘
Mating Edges: 5-Axis CNC Machined (±0.03 mm Seam Tolerance)
Alignment: Hardened Steel Locator Pins + Cam-Action Fast Locks
Sheet metal cabinets are manually cut, folded on press brakes, and welded in general fabrication shops.
The Good: Inexpensive to produce and easily customized to fit odd architectural dimensions.
The Bad: Sheet metal is heavy (often 40 to 50 kg per square meter), placing immense dead-load strain on your building’s structural steel. Worse, manual bending introduces mechanical tolerances of 0.5 mm to 1.0 mm. When you bolt twenty of these cabinets together, variances stack up, creating visible dark or bright seams across the screen. Furthermore, iron cabinets trap heat and require loud internal exhaust fans that rattle and fail over time.
Die-cast aluminum frames are molded under immense hydraulic pressure and finished on multi-axis computer numerical control (CNC) milling machines.
The Good: Extreme precision. CNC milling guarantees edge, corner, and locator-pin tolerances within ±0.03 mm to ±0.05 mm. Hardened stainless steel locator pins force adjacent cabinets into perfect planar alignment, eliminating visible seams. Aluminum is roughly 40% lighter (typically 24 to 30 kg per square meter), and the chassis acts as a passive heatsink, allowing completely fanless, silent operation.
The Bad: Initial procurement costs are 15% to 25% higher than sheet metal, but this is offset immediately by faster installation times and zero customer complaints regarding seam alignment.
Question: Front-service vs. rear-service cabinets—how do I decide which mechanical design to order?
Answer: This comes down entirely to physical installation access. If the display is installed on a freestanding highway pylon, an open-truss billboard, or a stadium structure with a rear catwalk, rear-service cabinets are mechanically simpler, cost less, and offer superior water protection because the front face is solid. However, if the sign is mounted flush against an exterior building wall, recessed into architectural brickwork, or installed inside a conference room, you must specify 100% front-service cabinets. Front-service modules unlock from the front face using a specialized magnetic extraction tool or front-release hex key, allowing a technician to replace a bad module, power supply, or receiving card in under two minutes without touching the back of the sign.
Question: What is the real-world difference between asynchronous and synchronous control systems?
Answer: A synchronous system requires a live, continuous video connection (such as HDMI, DisplayPort, or fiber) from a dedicated media player or PC; if the playback computer freezes or restarts, the screen goes dark. An asynchronous system (like the NovaStar Taurus TB-series or Colorlight A-series) is a standalone industrial micro-computer with internal solid-state memory. You upload schedules, videos, and text tickers over 4G cellular, Wi-Fi, or Ethernet. Once uploaded, the sign loops its stored programming independently. If the internet connection drops, the sign keeps running smoothly without missing a beat. For roadside advertising, gas station pricing, and school marquees, asynchronous cloud control is the clear industry standard.
Question: Can I purchase replacement modules from the same manufacturer three years from now and expect them to match my existing screen?
Answer: Physically, they will fit into the cabinet frames, but optically, they will almost certainly not match without extensive camera calibration. Semiconductor crystal growth is an organic chemical process; even the same manufacturer using the same packaging machines will produce diodes with slight variations in dominant wavelength and color temperature across different wafer batches. If you plug a new module into an older screen, it will stand out like an off-color patch. That is why you must contractually require the factory to supply a 5% batch-matched spare parts kit drawn from the exact same wafer lot as your primary shipment, and store those spares in a climate-controlled, static-safe space.
In our experience handling commercial installations, sign buyers frequently make the mistake of obsessing over pixel pitch while ignoring the mechanical mounting structure and local electrical codes.
Here are three rules we always recommend following:
First, never buy production quantities based on a glossy PDF catalog or digital renderings. Always order a fully functional 1-square-meter evaluation cabinet built to your exact bill of materials. Put that sample cabinet through its paces: check the solder joints under a microscope, measure the real power draw across full-white and dark screens with a calibrated power meter, test how the front-service latches hold up, and inspect the powder coating for pinholes.
Second, structure your payment terms around verified factory acceptance milestones. The standard international trade term is a 30% deposit to begin production, with the remaining 70% balance paid before ocean dispatch. Never wire that final 70% based on photos or prerecorded demo videos. Hire an independent inspection agency (such as SGS, QIMA, or a trusted local engineering rep) to visit the factory floor, verify that serial numbers match your specific batch, confirm the continuous 72-hour burn-in run, and supervise the crating process. That small inspection fee is the best insurance policy you will ever buy.
Third, specify high-grade power supplies and surge suppression. An outdoor display drawing thousands of watts in an open field is a prime target for lightning-induced electrical surges and utility grid fluctuations. Insisting on genuine Mean Well power supplies with built-in active power factor correction, paired with primary and secondary multi-stage surge protection devices (SPDs rated for at least 10kA to 20kA), will prevent utility spikes from frying your control hardware and eliminate over 80% of routine field service calls.
Working directly with established, engineering-driven wholesale led display screen manufacturers takes more diligence upfront than clicking "buy now" on a generic wholesale portal. But when your commercial display powers on smoothly, survives five consecutive winters without a single dark pixel, and earns praise from building inspectors and clients alike, that upfront discipline pays dividends for years to come.