English
If you're searching for wholesale cob led video wall manufacturers, chances are you've already hit a wall of supplier listings that all look suspiciously similar — same pixel pitches, same brightness claims, same "factory direct" promises. But here's the thing: not every company claiming to manufacture COB LED video walls actually owns the production line. Some are trading companies with polished websites and borrowed factory photos. Others are legitimate manufacturers but specialise in SMD panels and only recently added COB as a side line. And then there are the real COB specialists — the ones with dedicated clean rooms, flip-chip bonding equipment, and years of packaging process refinement behind them.
So how do you actually find the right one? What does a fair wholesale price look like? And what quality checkpoints should you be running before you commit to a bulk order? I've been sourcing LED displays from Chinese manufacturers for close to a decade, working with integrators and end-users across North America and Europe. Let me walk you through everything I've learned — the good, the bad, and the stuff that only shows up after you've taken delivery.
Before we get into manufacturer evaluation, let's make sure we're on the same page about what COB actually is and why it matters for your purchasing decision.
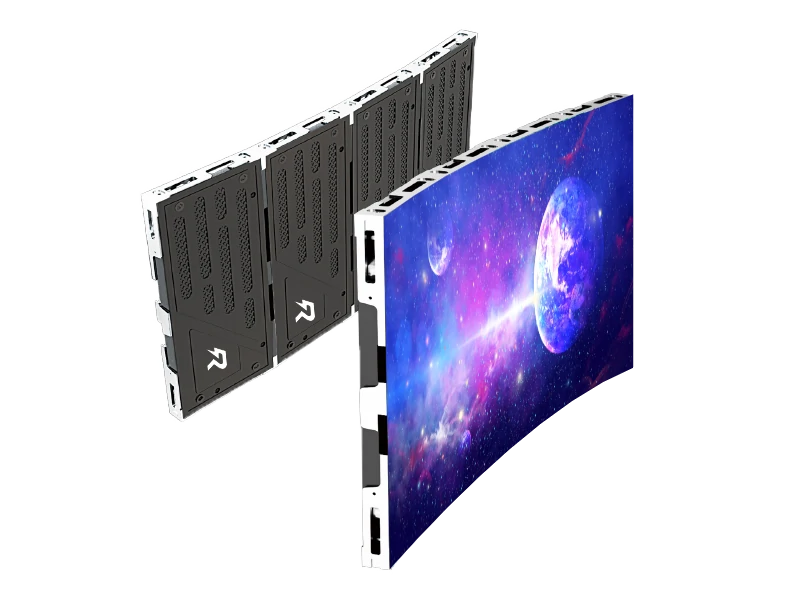
COB (Chip-on-Board) is a packaging method where bare LED chips are mounted directly onto a PCB substrate and then encapsulated with a protective epoxy or silicone compound — all as a single integrated module. This is fundamentally different from the traditional SMD (Surface-Mount Device) approach, where individual LED packages (each containing a chip inside a small plastic housing with solder pads) are soldered onto the PCB one at a time.
The practical differences this creates for your video wall are significant:
Durability — COB panels have no exposed solder joints or protruding LED packages on the surface. The entire face is a smooth, sealed plane that resists impact, dust, moisture, and static discharge. You can literally wipe a COB panel with a damp cloth. Try that with an SMD panel and you'll be picking broken LEDs out of the surface within a week.
Viewing comfort — The encapsulation layer acts as a built-in diffuser, producing a softer, more uniform light output that's easier on the eyes during prolonged viewing. This is why COB has become the default choice for control rooms, command centres, and conference rooms where people sit metres away from the display for hours at a time.
Contrast performance — COB panels typically achieve contrast ratios of 15,000:1 to 30,000:1 (with black matrix technology pushing even higher), compared to 3,000:1 to 5,000:1 for standard SMD panels. The sealed surface also eliminates the "sparkle" effect that SMD panels produce under mixed lighting conditions.
Pixel pitch range — COB technology currently dominates the sub-P2.0 fine-pitch segment, with mainstream products ranging from P0.6 to P1.8. This is where the technology's precision bonding capabilities give it a decisive advantage over SMD, which becomes increasingly difficult to manufacture reliably below P1.5.
This is the single most important skill you'll develop as a buyer in this space. The Chinese LED display market is absolutely packed with intermediaries who present themselves as factories. They'll have professional websites, factory tour videos, and sales teams that can quote specifications with confidence. But when it comes time to handle a custom engineering challenge or a warranty claim, you discover they have zero control over production. Here's my vetting process:
Not a pre-recorded marketing video. Not a virtual tour with background music. A real-time video call where you ask them to point the camera at specific equipment, show you the production line running, and walk through the bonding and encapsulation stations. Real COB manufacturers are proud of their clean room operations and will accommodate this without hesitation. If they stall, make excuses, or only offer pre-produced content — that's a significant red flag.
This is where you separate the real players from the pretenders. COB manufacturing requires precision die-bonding equipment that places bare LED chips directly onto the PCB substrate. The industry-standard machines come from manufacturers like ASM Pacific (now ASMPT), Kulicke & Soffa (K&S), and Shinkawa. Ask what brand and model of die bonder they operate. A genuine COB factory will have multiple bonding machines running in a clean room environment (typically Class 10,000 or better). If they can't name their equipment or show you the clean room, they're not manufacturing COB panels — they're buying finished modules from someone else and assembling cabinets.
After the chips are bonded, the panel goes through an encapsulation process where optical-grade epoxy or silicone is dispensed over the chip array and then cured under controlled temperature and humidity conditions. This step determines the optical quality, colour uniformity, and long-term reliability of the panel. Ask to see their encapsulation equipment and curing ovens. The curing process needs precise temperature profiling — rushed or poorly controlled curing leads to yellowing, delamination, and colour shift over time.
At fine pixel pitches (P1.2 and below), even minor brightness and colour variations between individual modules become visible when panels are tiled together into a video wall. Quality COB manufacturers use demura calibration systems from providers like Colorlight, Novastar, or Vivid to correct each module's uniformity at the pixel level. This equipment is expensive — typically $50,000 to $150,000 per system — and not every factory has it. Without proper calibration, your video wall will show visible colour patches and brightness inconsistencies, especially noticeable in dark or uniform content.
Every quality COB panel needs extended burn-in testing — typically 72 to 96 hours — after assembly. For indoor COB panels, the best factories run aging tests in temperature-controlled chambers at elevated temperatures (40°C to 50°C) to accelerate the detection of early-failure components. This catches latent defects that would otherwise turn into dead pixels or colour anomalies weeks after installation. No aging facility means no real quality gate, and that's a problem you'll discover the hard way.
Let me lay out what you should actually expect to pay when sourcing COB LED video wall panels from Chinese manufacturers at wholesale quantities. These are factory-gate prices for orders of 10 square metres and above:
| Configuration | Price per m² (USD) | Typical Application |
|---|---|---|
| P0.9 COB (flip-chip, 3840Hz, calibrated, front-service) | $2,200–$3,500 | Control rooms, broadcast studios, executive boardrooms |
| P1.2 COB (flip-chip, 3840Hz, calibrated, front-service) | $1,600–$2,600 | Conference rooms, command centres, luxury retail |
| P1.5 COB (flip-chip, 3840Hz, die-cast cabinet) | $1,100–$1,800 | Corporate lobbies, auditoriums, houses of worship |
| P1.8 COB (standard, 3840Hz, die-cast cabinet) | $850–$1,400 | Exhibition halls, large venues, education |
| P0.6 COB (MicroLED, premium calibration) | $4,000–$6,500 | Virtual production, premium broadcast, cinematic LED |
A critical note on what these prices do NOT include: Video processors and sending boxes, mounting structures (wall frames, floor stands, or recessed mounting frameworks), signal cabling (HDMI, fibre optic, Cat6), spare parts packages, shipping and freight, import duties and taxes. When you're budgeting a complete deployed system, plan to add roughly 45% to 70% on top of the panel-only cost for a fully functional installation. The exact percentage depends on the complexity of your mounting situation, the length of cable runs, and whether you need custom fabrication for structural supports.
I've watched buyers get excited about a quote that looks 30% cheaper than competitors, only to discover later that the lower price covered bare modules without cabinets or power supplies. Sometimes the "price per square metre" is calculated based on module area rather than cabinet area, which can be misleading when cabinets include bezels and framing. Always confirm in writing exactly what's included in any quoted price.
Here's where you'll see the biggest differences between manufacturers who take their COB production seriously and those who just assemble bought-in modules and slap a label on the finished product.
| QC Stage | What Gets Inspected | Consequence If Skipped |
|---|---|---|
| Incoming Chip Bin Sorting | Wavelength (±1nm), luminous intensity (±5%), forward voltage | Visible colour patches and brightness inconsistency across the wall |
| Post-Bonding AOI Scan | Chip placement accuracy, wire bond integrity, adhesive coverage | Intermittent dead pixels that appear weeks after deployment |
| Encapsulation Quality | Bubble-free surface, uniform thickness, proper curing profile | Yellowing, delamination, and optical distortion over time |
| Extended Burn-in (72-96hrs) | Full-colour cycling at elevated temperature, power supply stability | Latent LED and driver failures that show up after installation |
| Post-Assembly Calibration | Module-by-module brightness and colour correction via demura system | Visible seams, colour banding, and uneven brightness across tiled panels |
| Cabinet Flatness Test | Surface deviation ≤0.05mm across cabinet | Visible seams between cabinets when tiled into a video wall |
The encapsulation quality step is unique to COB manufacturing and it's where a lot of budget producers cut corners. The epoxy or silicone compound needs to be applied in a dust-free environment with precise thickness control. Bubbles trapped in the encapsulant create visible bright spots. Uneven thickness causes optical distortion and colour shift at different viewing angles. Improper curing leads to premature yellowing — I've seen panels from budget manufacturers develop a noticeable amber tint within 12 to 18 months of installation, completely destroying the colour accuracy.
This question comes up constantly, and the honest answer depends on your specific application. Let me break it down:
Best suited for fine-pitch indoor applications (P0.6 to P1.8) where viewers are close to the display, durability matters, and image quality is paramount. Think control rooms, conference rooms, broadcast studios, and premium retail environments. COB panels are more expensive per square metre than SMD at equivalent pixel pitches, but they deliver superior contrast, better eye comfort, and significantly higher physical durability.
Still the dominant technology for coarser pixel pitches (P2.0 and above) and outdoor applications where extreme brightness is needed. SMD panels are cheaper to produce at larger pixel pitches and offer higher maximum brightness for outdoor use. If your application doesn't require sub-P2.0 resolution and you're not in a high-touch environment, SMD remains a perfectly valid and cost-effective choice.
A hybrid approach where a protective glue layer is applied over a traditional SMD panel. GOB gives you some of the surface protection benefits of COB (impact resistance, dust/moisture sealing) at a lower cost point than full COB. However, GOB doesn't achieve the same optical quality or contrast performance as true COB because the underlying LED packages still create light scattering at the chip level. GOB is a reasonable middle-ground option for applications where you need better durability than bare SMD but can't justify full COB pricing.
Choosing the right pixel pitch for your COB video wall comes down to three factors: the closest viewing distance, your budget, and whether the wall will be captured on camera for broadcast or live streaming.
P0.6 to P0.9 — Ultra-premium choice for viewing distances under 1.5 metres. Used in virtual production volumes, premium broadcast studios, and executive boardrooms where the display replaces a large-format monitor. Highest cost per square metre in the COB category. At P0.9, a standard 16:9 4K resolution requires approximately 3.5 square metres of display area.
P1.2 to P1.5 — The sweet spot for most corporate and institutional COB installations. Handles viewing distances of 1.5 to 3 metres comfortably. Excellent balance of resolution, cost, and availability. This is where you'll find the deepest manufacturer competition and the best value for money. A 16:9 4K display at P1.25 requires approximately 6 square metres.
P1.8 — Budget-friendly COB option for larger venues where the closest audience is 3+ metres away. Lower resolution than P1.2 but still significantly sharper than SMD at equivalent pitches. Good choice for auditoriums, exhibition halls, and houses of worship where the display is viewed from a distance.
This is the number one issue I see across all COB purchases. LED chips are sorted into "bins" based on their wavelength, brightness, and forward voltage. At fine pixel pitches, even a small wavelength difference between bins becomes visible when panels are tiled together. You need to specify in your purchase agreement that all panels must come from the same LED wavelength bin (±1nm) and the same brightness bin (±5% intensity variation). Some manufacturers will default to wider bin tolerances to improve their yield and lower costs, which means you might get panels that look fine individually but show visible colour patches when assembled into a video wall.
For any installation that will be captured on camera — corporate presentations recorded for internal distribution, broadcast studios, virtual production, conference rooms with video conferencing — you need a minimum refresh rate of 3840Hz. Lower refresh rates cause visible flickering and scan lines on camera. Some manufacturers quote COB panels at 1920Hz as standard because it's cheaper to produce, and they'll only upgrade to 3840Hz if you specifically ask. Always confirm the refresh rate in your written specifications and verify it with a camera test upon receipt.
At fine pixel pitches, viewers are close enough to notice even tiny misalignments between cabinets. The die-cast aluminium cabinets need machining tolerances of ±0.05mm (tighter than the ±0.1mm acceptable at P2.0 or P2.5). The magnetic or mechanical connection between cabinets needs to pull panels together with consistent force to eliminate any visible gap or height difference. Ask the manufacturer for their cabinet-to-cabinet seam specification — it should be ≤0.05mm gap and ≤0.05mm height difference for fine-pitch COB installations.
COB panels are often installed in recessed or flush-mounted configurations where airflow is restricted. This creates a thermal trap that accelerates LED degradation and can cause premature colour shift. If your installation design involves recessed mounting, make sure the manufacturer's cabinets have adequate ventilation paths and that you're not exceeding the recommended maximum ambient temperature (typically 40°C for indoor COB panels). Some manufacturers offer enhanced thermal management packages with additional heat sinks or low-noise fans for recessed installations — worth the investment if your design constrains airflow.
COB panels are almost universally designed for front-service access because they're typically installed flush against a wall or in a recessed cavity where rear access is impossible. This means you need to confirm that the manufacturer's cabinet design allows individual modules to be removed and replaced from the front using magnetic pull tools or similar mechanisms. I've seen installations where a single faulty module required the entire wall section to be dismantled because the manufacturer used a rear-service design that was completely inappropriate for the mounting configuration.
The panel price is just the starting point. Here's what else goes into the total cost when importing COB LED video wall panels from Chinese manufacturers:
Freight: Sea freight (FCL) is the most economical option for orders over 5 square metres. COB panels are typically shipped in flight cases or reinforced cartons with foam cushioning. A 20-foot container holds approximately 15 to 25 square metres of COB panels depending on cabinet size and packaging, with transit times of 15 to 25 days to the US West Coast and 25 to 35 days to European ports. Air freight delivers in 5 to 7 days but costs 4 to 6 times more — usually only justified for urgent replacement panels or sample shipments.
Import duties: COB LED display panels generally fall under HS code 8528.59. In the United States, standard duty sits around 0% to 5%, but Section 301 tariffs on Chinese-origin products can add an additional 25%. In the EU, standard duty is approximately 1.4% plus VAT. These rates shift periodically, so always verify with a licensed customs broker before finalising your budget.
Spare parts: Here's something I recommend to every buyer — when you place your initial order, simultaneously order a spare parts package equal to 5% to 8% of your total panel quantity. This should include extra modules from the same LED production batch, spare power supplies, additional receiving cards, spare ribbon cables, and extra magnetic pull tools for front-service access. Having matched spare parts on hand prevents a single failure from becoming extended downtime while you wait for an international shipment. For mission-critical installations like broadcast studios or control rooms where downtime is unacceptable, I'd push this to 8% to 12%.
Most COB panels ship with receiving cards pre-installed. The major control system ecosystems you'll encounter include Novastar (most widely adopted globally, excellent value, broadest hardware compatibility), Colorlight (strong cost-performance ratio, growing ecosystem), and Brompton Tessera (premium choice for broadcast, virtual production, and high-end rental). Make sure the receiving card model in your quote matches your preferred control system. Mixing ecosystems can work but adds unnecessary complexity and potential compatibility headaches.
For COB panels specifically, I'd recommend confirming that the receiving card supports 16-bit or higher grayscale processing. COB panels are often chosen for their superior contrast and colour depth, and pairing them with a receiving card that only processes 8-bit or 12-bit grayscale will bottleneck the image quality and waste the investment you've made in premium COB technology.
The wholesale relationships that deliver the best results over time are built on a few principles I've seen work consistently:
Start with a trial order — 3 to 5 square metres is enough to evaluate panel quality, communication responsiveness, documentation accuracy, and logistics reliability before committing to a full video wall installation.
Lock in LED bin specifications for repeat orders — once you've received and approved your initial batch, the manufacturer should record the exact LED bin codes and reserve matching stock for your future orders. This is the single most effective way to solve the colour consistency problem across multiple purchases.
Establish clear quality acceptance criteria in writing — dead pixel limits (I'd suggest ≤2 dead pixels per module as a starting point for COB), brightness uniformity tolerance (≤5% deviation across the panel), colour temperature range (±100K), and seam specifications. Don't leave these to verbal agreements.
Visit the factory if possible — even a single in-person visit transforms the relationship from transactional to collaborative. You'll see things on the production floor that no video call can show you, and the manufacturer will treat your account differently once they've met you face to face.
Provide feedback on field performance — manufacturers genuinely value customers who report how panels perform after 6, 12, or 24 months of real-world operation. This information helps them improve their products and gives you leverage for better terms on future orders.
When you become a repeat customer, several advantages kick in: priority production scheduling during peak season (Q3 through Q4 when the commercial AV industry is busiest), consistent LED batch allocation for colour consistency, custom engineering support for non-standard configurations like curved walls or ultra-wide aspect ratios, better payment terms (moving from 100% upfront to 30% deposit / 70% before shipment), and dedicated account management instead of rotating through different sales reps.
From where I sit, the wholesale COB LED video wall market is at a genuinely interesting inflection point. Production costs have dropped meaningfully over the past few years as flip-chip bonding processes have matured, encapsulation materials have improved, and manufacturing yields have climbed. But quality variation between manufacturers has actually widened at the same time. You've got factories producing COB panels with image performance and build quality that rival displays costing two or three times as much from Western brands, and you've got low-end workshops churning out panels that look fine on a spec sheet but can't hold colour uniformity across a multi-cabinet installation or survive two years without visible yellowing.
What I'd suggest to anyone exploring options right now: shortlist 3 to 5 manufacturers that meet the basic criteria I've outlined above, request sample cabinets from each, and do a direct side-by-side comparison. Run the same content on all of them. Look at the seams between cabinets. Check the colour uniformity across a large white field. View the panels through a camera at different shutter speeds to test refresh performance. Leave a sample in direct sunlight for a month and check for any encapsulant degradation. The differences become really obvious once you have physical panels in front of you running the same content, and that hands-on evaluation is worth far more than any amount of spec-sheet comparison or online research.
The extra time you put into proper evaluation upfront will pay for itself many times over in reduced field failures, longer panel lifespan, and fewer project emergencies. COB LED video wall technology is mature and capable of delivering excellent performance for a decade or more — as long as you partner with a manufacturer who takes the engineering seriously and has the production infrastructure to back up their claims.
Most manufacturers set their wholesale pricing threshold at 5 to 10 square metres. Some will accommodate smaller trial orders of 2 to 3 square metres at a slightly higher per-unit cost. True volume wholesale pricing with the best per-square-metre rates typically kicks in at 15 to 20 square metres and above.
Well-manufactured COB panels carry a rated lifespan of 80,000 to 100,000 hours, which translates to roughly 9 to 11 years of continuous 24/7 operation. In typical commercial use running 8 to 16 hours daily, you can expect 15 to 20+ years before brightness degrades to 50% of original output. COB's sealed encapsulation actually extends real-world lifespan compared to SMD because the chips are protected from dust, moisture, and physical contact.
Request a live video factory tour, verify they own their die-bonding equipment (ASM, K&S, or Shinkawa machines), confirm in-house encapsulation and curing lines, check for a dedicated demura calibration system, and ask for verifiable certifications (CE, FCC, RoHS, ETL/UL). Real manufacturers will accommodate all of these requests without hesitation.
Industry standard warranty is 2 to 3 years covering manufacturing defects in LED chips, driver ICs, power supplies, and PCB boards. Some premium manufacturers offer extended warranty packages. Always confirm whether the warranty covers on-site replacement service or requires return-to-factory repair, and whether labour costs for field replacement are included.
Request that all panels be produced from the same LED wavelength bin (±1nm) and same brightness bin (±5%). Reputable manufacturers maintain detailed batch records and can match repeat orders to your original LED bin specification. Always order spare modules from the same production batch as your main order to guarantee visual consistency.
Standard COB panels are designed for indoor use. However, some manufacturers now offer outdoor-rated COB panels with IP65 front protection and enhanced UV-resistant encapsulation materials. These are significantly more expensive than indoor COB panels and are primarily available in P1.5 to P2.5 pixel pitches. If you need outdoor capability, confirm the IP rating and UV resistance specifications in writing.
Most COB panels work with all major LED control systems. The most common are Novastar (most widely adopted globally), Colorlight (strong cost-performance ratio), and Brompton Tessera (premium choice for broadcast and virtual production). Specify your preferred control ecosystem when ordering so the manufacturer installs the correct receiving card model.
Quality COB panels typically require 25 to 40 working days depending on the pixel pitch and order size. Fine-pitch panels (P0.9, P1.2) with full demura calibration may take 30 to 40 working days due to the more rigorous QC process. During peak season (Q3 to Q4), add another 5 to 10 working days. Always confirm the lead time in writing and build buffer time into your project schedule.
At minimum, look for CE (European conformity), FCC (US electromagnetic compatibility), RoHS (restriction of hazardous substances), and ISO 9001 (quality management system). For North American installations, ETL or UL listing is often required by local building codes and insurance requirements. Always verify certifications independently through the issuing body's official database rather than accepting PDF copies at face value.
COB and MicroLED are related but distinct technologies. COB refers to the packaging method (chips bonded directly to PCB and encapsulated), while MicroLED refers to the chip size (typically under 50 micrometres). Many current COB panels use chips in the 100 to 200 micrometre range — technically mini-LED by size classification. True MicroLED (sub-50μm) is still in early commercialisation and commands a significant price premium. For most current video wall applications, COB with mini-LED chips (P0.9 to P1.8) offers the best balance of performance, availability, and cost.